PLC ENGINEERING

Siemens S7-300

Home

Siemens S7-300

  • Siemens S7-300 Analog Input Troubleshooting: SM331 Faults Found in the Field
    Siemens S7-300 Analog Input Troubleshooting: SM331 Faults Found in the Field Aug 24, 2026
      Three in the morning. The packing line goes quiet. Not the graceful quiet of a planned stop. The kind that makes the night operator call me with a voice that says this is not the first problem tonight. "The tank level reads full," he says. "Full and climbing. We're about to put product on the floor." I pull up the VAT table on my laptop. The raw word for the level channel sits at 27648. Pegged hard at the top of the scale. The transmitter on that tank is a 4-20 mA unit, and 27648 is what the SM331 reports when the input is maxed out. Either the tank really is overflowing, or something in that loop is lying. It was the loop. It usually is. I've replaced more SM331s than I can count. I've also watched perfectly good modules get condemned because a 2-wire transmitter got wired into a slot set up for 4-wire, or a range card went back in backwards after a panel cleaning. Nine times out of ten it's not the module. It's the stuff hanging off the terminals. This article is the order I check things in, ranked by how often I actually see each fault in the field. Work the list top to bottom before you order a spare. You'd think the module is the problem. Most nights, it isn't.   What the SM331 Actually Is   The SM331 is the analog input card for the S7-300 family. It takes the 4-20 mA, 0-20 mA, or voltage signal from a field transmitter and turns it into a number the CPU can use. That number is a raw integer between 0 and 27648 for unipolar ranges, or between -27648 and +27648 for bipolar ranges. The CPU then scales that raw value into engineering units: percent, bar, or degrees Celsius. Whatever the process needs. The whole family shares a few traits. They mount on the same rail. They use the same backplane bus. They all answer to the same diagnostic system. The differences are in the channel count, the resolution, the input ranges, and how well the channels are isolated from each other. One thing I tell every apprentice: an SM331 is a dumb, honest device. It does not invent readings. If it reports 27648, something drove the input there. If it reports zero, the loop is open or dead. The card is a voltmeter with a serial number. Treat it that way and troubleshooting gets a lot simpler.   SM331 Models You'll Meet in the Field   Not all SM331s are the same. The order number tells you almost everything. These are the ones I actually see in plants, with what they're good for. Order number | Channels | Resolution | Input ranges | Typical use 6ES7331-7KF02-0AB0 | 8 AI | 12-bit | 0-20 mA, 4-20 mA, ±10 V | The workhorse. Process signals, transmitters, drive feedback 6ES7331-7KB02-0AB0 | 2 AI | 12-bit | 0-20 mA, 4-20 mA, ±10 V | Small panels, a couple of signals, retrofits 6ES7331-7NF10-0AB0 | 8 AI | 15-bit | 0-20 mA, 4-20 mA, ±10 V | High resolution, precision weighing, fast loops 6ES7331-7NF00-0AB0 | 8 AI | 15-bit | 0-20 mA, 4-20 mA, ±10 V | Older high-res card, same job as the 7NF10 6ES7331-1KF02-0AB0 | 8 AI | 13-bit | 0-10 V, ±10 V, 0-20 mA | Voltage-heavy panels. No isolation between channels 6ES7331-7PF11-0AB0 | 8 AI | 16-bit | RTD, thermocouple | Temperature. Pt100, type J and K A few notes from the field. The 7KF02 is the one you'll pull out of most racks. It's cheap, it's everywhere, and the range card lets one card handle voltage, current, and on some positions even Pt100 and thermocouples. That flexibility is why it survived so long. The 1KF02 has no isolation between channels. Every channel shares the same reference. A ground fault in one loop drags the whole card. I've seen one bad field cable take down all eight channels at once, and the maintenance crew replaced two perfectly good cards before somebody checked the cable. The 7NF10 uses a 40-pin front connector. The 7KF02 and the 1KF02 use 20-pin. When you buy a replacement, match the connector, or you'll be hunting for the right cable at 2am.   The Fault List, Ranked by How Often I See It   1. Wiring and Polarity   This is the big one. I'd say half of my analog calls end with a screwdriver fix, not a parts order. The most common mistake is reversed polarity on the channel terminals. M+ and M- swapped. An instrument tech re-terminates a pressure transmitter after a calibration, gets the pair crossed, and the reading dies. The operator swears the transmitter is dead. The transmitter is fine. The two little letters on the terminal block are the whole story. Current inputs need a return path. If the negative side of the loop is floating, you get garbage. Not zero, not pegged. Garbage. Values that wander around like a drunk man. I've also seen a terminal that looked tight but had a strand of wire hanging by a thread. The reading dropped every time the machine vibrated. You'd think it was a loose sensor. It was a loose screw. Checks: · Are the terminal screws actually tight? Pull on each wire, not gently. · Is M+ on the module going to the plus side of the signal? Is M- going to the minus? · Does every current channel have a complete return path? · Any corrosion, green fuzz, or discolored terminals in wet areas? Fix: re-terminate with ferrules, replace damaged terminal blocks, and label the pair. A label costs ten seconds and saves an hour.   2. Two-Wire vs Four-Wire Transmitters   This one sends good modules to the scrap bin. A 2-wire transmitter is powered by the loop itself. The module has to be configured for 2-wire operation so it feeds loop power out of the channel. A 4-wire transmitter runs on its own supply. Its output is just a signal, and the module only measures it. Wire a 2-wire transmitter into a slot configured for 4-wire and there is no loop power. The card reads zero. Everybody blames the card. I found a brand-new pressure transmitter like that once, installed by a contractor, dead on arrival according to the foreman. It took me two minutes with a multimeter to find the loop had no voltage on it. The card never had a chance. The reverse is worse. Wire a 4-wire transmitter into a slot configured for 2-wire and the module tries to drive loop current into an output that can't sink it. The reading pegs at 27648 and the transmitter output stage gets hot and unhappy. That's the "tank is full" call at 3am, sometimes with a genuinely full tank because the valve closed on a false reading. Checks: · How many wires go to the transmitter? Two means 2-wire. Four means it has its own power pair. · What does the HW Config entry say for that channel group? · What position is the range card in? Fix: set the range card and the HW Config to match the transmitter type, and land the loop supply where it belongs.   3. Raw Value Stuck at 27648 or 0   The classic. A raw value pinned at 27648 means the input is being driven to maximum. A raw value pinned at 0 means the loop is open, the sensor is dead, or the supply is missing. Both look identical on the HMI: a bad reading. Both have completely different causes. Pegged at 27648, in order of likelihood: the sensor is shorted or pegged, the loop current really is above 20 mA, the transmitter output is saturated, or the range is set wrong. I had a tank level that read full for a week. The operator wrote it off as a faulty card. The cable had been pinched under a cable tray during a roof job, shorting the pair together. The transmitter was pushing its maximum against a shorted loop. The card was reporting the truth. Stuck at 0: an open loop, a dead transmitter, a blown fuse on the 24V loop supply, or a wire break with monitoring turned off. And here's a subtle one: if the channel is configured for 0-20 mA but the transmitter is 4-20 mA, the card reads about 20% of scale when the tank is empty. Not zero. Twenty percent. Operators call that "leaking" and it's a config problem, not a hardware problem. Checks: · Put a mA meter in series with the loop. What does the current actually read? · Measure voltage across the transmitter terminals. Is it getting what it needs? · Check the 24V rail and the loop fuse. Fuses die at 3am more than any component. Fix: replace the fuse, repair the cable, or replace the sensor. Then inject 12 mA with a loop calibrator. If the card reads mid-scale, the card was never the problem.   4. Channel Group Isolation Faults   The 7KF02 isolates its channels in groups of two. Channels 0 and 1 share a group. So do 2 and 3, 4 and 5, 6 and 7. When one channel in a group takes a hit, its partner rides along. I've seen a surge take out the input protection on channel 0, and channel 1 read nonsense for a month while everybody blamed the transmitter on channel 1. The group wiring also shares the reference. A shorted field cable on one channel in the group can pull the group's reference and drag the neighbor's reading. Same group, same fate. Checks: · Move the suspect signal to a channel in a different group. If it reads fine there, the group is damaged, not the whole card. · Check both channels in the group. If they both misbehave, suspect the group. · Look at the field cable on both channels, not only the one that's alarming. Fix: repair the faulted field path. If the input stage of that group is genuinely blown, the card has to go. You can't bypass a dead group.   5. Wrong Range Module or Wrong Setting   The 7KF02 has a range card, a little board you slide into the front of the module. It sets the measurement range for each channel group. It can go in backwards. It can go into the wrong slot. I watched a panel cleaning crew pull one, wipe the contacts, and put it back rotated 180 degrees. Half the channels read nonsense after that. Nobody touched the program. Nobody touched the wiring. A $5 piece of plastic was the whole fault. The range card position and the HW Config entry have to agree. If the card says 4-20 mA but HW Config says 0-10 V, the readings will be wrong in a way that looks like a sensor problem. And the order number and hardware version in HW Config have to match the actual module, or the CPU flags the slot. Checks: · Pull the range card. Is it the right way around? Is it in the right position? · Does HW Config show the same range for that group? · Does the order number in HW Config match the module in the rack? Fix: reinsert the card correctly, correct the HW Config entry, and download. Reboot the rack if the CPU is grumpy about it.   6. Grounding and Common-Mode Voltage   The 7KF02 only separates its channel groups by about two volts. That is not real isolation. It's a token separation. If the transmitter and the PLC sit on different ground potentials, the difference lands right on the input. Readings drift. They jump. Sometimes they peg. I had a compressor skid built in the States, running 120V/60Hz, sitting next to a 230V/50Hz plant panel. The analog signal drifted all day long. The grounds disagreed by a couple of volts and the 7KF02 had no headroom for it. The fix was a single-point ground and a shield grounded at one end. The 15-bit 7NF modules handle this kind of thing better, but you can't always pick your hardware. Checks: · Measure the voltage between the transmitter negative and the module M- terminal. More than a volt or two is a common-mode problem. · Is the shield grounded at both ends? That's a ground loop with a hum. · Are the signal cables sharing a tray with motor leads or VFD cables? Fix: single-point grounding, one end of the shield grounded and the other taped, and in stubborn cases an isolator between the transmitter and the card. It costs less than a new module and it fixes the root cause.   7. Addressing and Slot Configuration   The module is in slot 4 and the config says slot 5. Or the order number in HW Config doesn't match the card that's actually installed. The CPU either faults the slot or the values never update. The HMI shows stale numbers and the operators think the process is frozen. I've also been handed a "new" module from stores that was an older hardware version than what HW Config expected. The CPU refused to accept it. The fix was matching the version in the config to the card in the rack, or finding the right card. Check the input word addresses too. An 8-channel card takes eight words, and if two cards overlap on addresses, you get readings that fight each other. Checks: · Open Module Information in HW Config. Does the card report the order number and version you expect? · Is the module in the slot the config says it's in? · Do the input word addresses overlap with another card? Fix: correct the config, download, and confirm the addresses. Then verify the live value in a VAT table.   8. The Module Is Actually Dead   Last on the list, and it should be. Real hardware failure happens. A surge takes out an input stage. A shorted transmitter pumps 24V into an input that was only rated for milliamps. Lightning lands on a fence line a hundred meters away and the whole rack flinches. Sometimes a card just dies of old age. The signs are honest: SF LED steady on, Module Information showing an internal fault, no channel responding even with a calibrator directly on the terminals, and the fault follows the card when you move it to another slot. If you've done steps 1 through 7 and the card still won't behave, it's the card. Checks: · Swap test with a known-good card. Fault follows the card? It's the card. · Smell the module. Burnt electronics have a distinctive smell. So does a blown input protection stage. · Look for visible damage on the input circuitry. Fix: replace it. Match the order number exactly and check the hardware version against your HW Config entry. A used 6ES7331-7KF02-0AB0 from a reputable supplier is fine. Just confirm the version and that the range card comes with it. Front connector type matters too. If you're shopping, we carry Siemens PLC spare parts and general PLC spare parts that cover the common SM331 versions, new and used. New modules carry CE and UL markings. Used ones from the EU or the States are fine as long as the order number and version match.   Diagnostics: What the Card Is Telling You   The SF LED   The SF LED is the module's whole vocabulary. Learn it and you skip half the guesswork. LED state | Meaning | What to do SF off | No fault reported by the card | Trust it, but still check the field wiring SF flashing | Channel fault: wire break, overrange, underrange | Read the diagnostics, find the channel SF steady on | Parameter assignment error or internal fault | Check HW Config, range card, and module version   Reading Module Information   In HW Config, double-click the module and open Module Information. The Diagnostics tab is where the card tells the truth. It names the channel, the fault type, and whether it's a wire break, an underrange, or an overrange. It also shows internal faults that the LEDs can't express. If you enable the diagnostic interrupt in the module parameters, the CPU gets notified on every fault. That's where the trap is. If the interrupt is enabled and OB82 is not loaded in the program, the CPU goes to STOP the first time a channel faults. I've answered that call at 3am. Someone enabled diagnostics for a good reason and forgot the OB. The whole line stopped because one spare channel had a loose wire.   Watching the Raw Value   Open a VAT table and enter the input word address. For an 8-channel card, that's eight words. Watch the value while you inject a known signal at the field terminals. If the raw value follows the signal, the card and the config are fine. If the raw value ignores the signal, work back toward the field, terminal by terminal.   Wire Break Monitoring   Wire break monitoring is parameterizable on the 4-20 mA and 1-5 V ranges. When it's on, an open loop reads 32767 and the SF LED flashes with a wire break diagnostic. When it's off, an open loop reads 0 and looks exactly like a dead sensor. Know which setting you have, or you'll chase a ghost for an hour.   Raw Value to Engineering Units   Here's the map I keep in my head. Raw values are integers, and the scale is fixed. Raw value | Percent of range | 4-20 mA signal | What it usually means 32767 | overrange | above 20 mA | Wire break with monitoring on, or overrange 27648 | 100% | 20 mA | Input maxed. Sensor pegged, short, or wrong range 20736 | 75% | 16 mA | Normal reading at 75% 13824 | 50% | 12 mA | Mid-scale. Normal 6912 | 25% | 8 mA | Normal reading at 25% 0 | 0% | 4 mA | Zero signal, open loop, or dead transmitter -32768 | underrange | below 4 mA | Underrange with monitoring on One thing that trips people up: on the 4-20 mA range, the module maps 4 mA to raw 0 and 20 mA to raw 27648. The dead zero of the 4-20 range is already removed inside the card. So when you scale, the low limit is the engineering value at 4 mA, not the value at 0 mA. Get that backwards and your tank reads full when it's empty.   Scaling with FC105   FC105 is the SCALE function in the standard library. IN is the raw integer from the input word. HI_LIM and LO_LIM are your engineering range. BIPOLAR tells the block whether the raw range is -27648 to +27648 or 0 to 27648. OUT is the real result. RET_VAL is the status word, and you should check it. If it's not zero, the conversion has a problem. Most scaling bugs I see are a wrong BIPOLAR flag or swapped limits. Both produce readings that are wrong in a very consistent way, which makes operators trust them more, not less. A reading that's always 10% high is a scaling bug until proven otherwise.   Wiring It Right   2-Wire Hookup   The module feeds the loop power. L+ lands on the module's L+ terminal. The loop current comes out of the channel's M+ terminal, through the transmitter, and back into M-. No external supply needed. If the module isn't configured for 2-wire, there's no loop power and the reading sits at zero, waiting for you to blame the card.   4-Wire Hookup   The transmitter runs on its own supply. The signal pair goes to M+ and M-. Do not feed loop power from the module into a 4-wire transmitter output. The card pegs and the transmitter output stage gets hot. I've replaced two transmitters before I found a contractor doing exactly that.   Shielding   Twisted shielded pair for 4-20 mA, always. Ground the shield at one end only. Pick the panel end or the field end and stay consistent. Both ends grounded is a ground loop with a nice hum. Keep signal cables out of the tray with the motor leads and the VFD cables. I've seen a VFD turn a clean 4-20 mA signal into noise you could hear on a radio. The card reads it as a signal. The process reads it as chaos.   Fixes, in Order   · Terminals: tight, clean, ferruled, with M+ and M- correct. · Loop: meter in series, confirm the current matches the process. · Supply: 24V at the loop, fuse good, polarity right. · Config: range card position, HW Config order number, hardware version, measurement range. · Isolation: move the signal to another channel group, inject with a calibrator. · Then the card. Do it in that order and you'll replace a lot fewer modules. I keep a loop calibrator in my truck. It has paid for itself a hundred times over. A $200 tool that proves the card is fine is cheaper than a $400 module that isn't the problem.   When to Replace the Module   Replace the module when the SF LED is steady on with an internal fault in diagnostics. Replace it when no channel responds, even with a calibrator directly on the terminals. Replace it when the fault follows the card to another slot. Replace it when you can smell burnt components. Surge damage on an input stage is not repairable on the floor. Don't waste a shift on it. When you buy the replacement, match the order number exactly. Check the hardware version against your HW Config entry. Confirm the front connector type. Confirm the range card is included. A module without its range card is a paperweight on the 7KF02. We stock Siemens PLC spare parts with the versions listed, so you can match before you order instead of after.   Maintenance Checklist   · Every shutdown: check terminals for tightness and corrosion. · Pull the range card, inspect the contacts, reinsert it correctly. · Verify shield grounds are single-ended. · Log raw values for healthy channels so you know what normal looks like. · Check the 24V rail and the loop fuses.
  • Siemens S7-300/400 Memory Concept Explained: Load Memory, Work Memory, and Retentive Data
    Siemens S7-300/400 Memory Concept Explained: Load Memory, Work Memory, and Retentive Data Aug 18, 2026
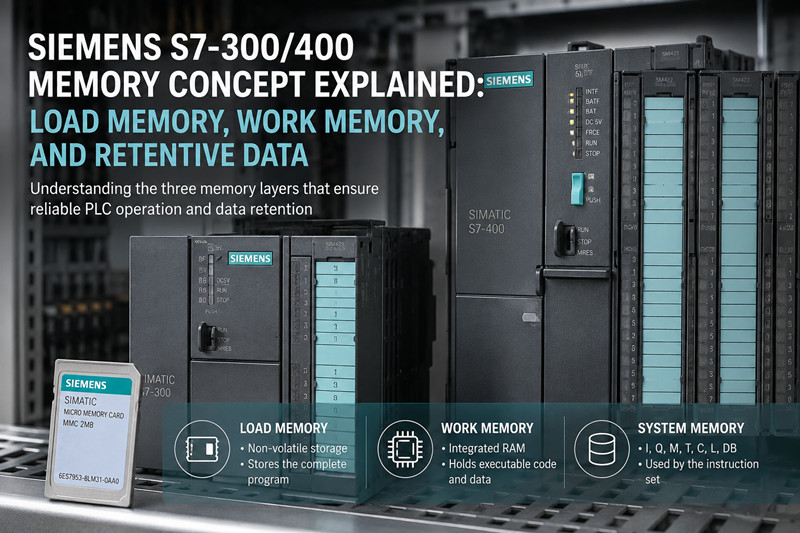
      The memory architecture of the Siemens S7-300 and S7-400 programmable logic controllers is organized into three distinct layers: load memory, work memory, and system memory. Every memory-related fault, whether a CPU that refuses to leave STOP, a program that disappears after a power outage, or a battery alarm on an S7-400, can be traced back to one of these layers and to the rules that govern how data moves between them. This article defines each layer precisely, explains how the two controller families implement them differently, provides the concrete parameters of representative CPUs, and closes with failure diagnostics, maintenance practice, and the questions that engineers most frequently search for. The material assumes a working knowledge of STEP 7 and of the general structure of a PLC program, but no prior specialization in memory management.   1. The Three Memory Layers Defined   Load memory holds the complete user program, including code blocks (OB, FB, FC), data blocks (DB), symbols, comments, and technology data. It is the non-volatile, or battery-backed, repository from which the CPU restores its working copy at every startup. Work memory is the integrated RAM area in which the CPU actually executes the program; it contains only the code and data required for execution. System memory is the set of address areas that the instruction set operates on: process inputs (I), process outputs (Q), bit memory (M), timers (T), counters (C), local data (L), and data blocks (DB). The distinction between the three layers is not academic. A block that exists only in load memory is not executed. A block that exists only in work memory is executed but cannot be uploaded to a programming device. A retentive flag that is not backed up in load memory is reset at every restart. Each layer has its own volatility, its own capacity limits, and its own failure behavior, as summarized in Table 1. Table 1: The three memory layers at a glance Layer | Contents | S7-300 implementation | S7-400 implementation | Behavior on power loss Load memory | Full program: blocks, symbols, comments, technology data | Micro Memory Card (MMC) | RAM backed by battery; optional Flash EPROM card | S7-300: retained on the MMC. S7-400: retained in RAM while the battery is healthy; otherwise restored from EPROM or lost Work memory | Executable code and data only | Integrated RAM | Integrated RAM | Contents lost; rebuilt from load memory at the next startup System memory | I, Q, M, T, C, L, DB addressing | Internal CPU circuitry | Internal CPU circuitry | Non-retentive parts reset; retentive parts restored from load memory A second axis runs through the architecture: the difference between volatile and non-volatile storage. On the S7-300, non-volatility is achieved with flash memory (the MMC) and no battery is required. On the S7-400, non-volatility is achieved with a battery-backed RAM and, optionally, with a Flash EPROM card. This single difference explains most of the practical divergence between the two families, from the battery-low LED on the S7-400 to the fact that an S7-300 CPU without an MMC will not start at all.   2. Load Memory: Where the Program Is Stored   Load memory is the highest-capacity layer. It stores the program in its complete form, including data that the CPU never executes directly: block comments, symbol information, and technology objects. When a project is compiled and downloaded, every block is transferred into load memory first. The CPU then copies the executable portions into work memory. Because load memory holds the full project, it is also the layer that an upload reads when you transfer a program from a CPU back to a programming device.   2.1 Load memory on the S7-300: the Micro Memory Card   All current S7-300 CPUs store load memory on a Micro Memory Card (MMC). The MMC is a plug-in flash card that fits into a slot on the front of the CPU. It requires no battery, which is why an S7-300 plant can sit without power for years and still start with its program intact. Representative order numbers for the MMC family are 6ES7953-8LL31-0AA0 (512 KB) and 6ES7953-8LM31-0AA0 (2 MB); the same family extends from 64 KB up to 8 MB, and the maximum acceptable size depends on the CPU. The MMC is not an optional accessory. A modern S7-300 CPU without an MMC cannot run a program: the CPU goes to STOP and requests a memory card in the diagnostics buffer. This is a deliberate design decision. Because the MMC is the only non-volatile storage in the system, it holds not only the program but also the retentive data and, on some CPUs, the firmware. If the card is missing, the CPU has neither a program to execute nor a place to store retentive state. The MMC carries a small write-protection slider on its housing. When the slider is in the locked position, the CPU rejects downloads with a message stating that the memory card is write-protected. The slider protects the card against accidental overwrite in the field, but it is a common cause of failed downloads after maintenance, so its position should be the first thing checked when a download is refused. If load memory is lost or empty: on the S7-300, an empty or missing MMC means the CPU stops and cannot start. On the S7-400, an empty RAM load memory with no EPROM card means the CPU starts into STOP with no user program; if an EPROM card is present, the CPU copies the program from the EPROM into RAM at startup and runs normally.   2.2 Load memory on the S7-400: battery-backed RAM and Flash EPROM   The S7-400 implements load memory in two stages. The primary stage is RAM integrated on the CPU module, which holds the working copy of the load memory. This RAM is kept alive by a backup battery, for example 6ES7971-0BA00, mounted in the power supply or in the CPU compartment. The secondary stage is a plug-in Flash EPROM card, for example 6ES7952-1KM00-0AA0, which provides non-volatile storage that survives even a complete loss of battery power. At power-up, the S7-400 behaves as follows. If the RAM load memory contains a program, the CPU copies it into work memory and starts. If the RAM is empty but a Flash EPROM card is inserted, the CPU copies the program from the EPROM into the RAM load memory and then into work memory. If both are empty, the CPU goes to STOP. This startup chain is the reason why a well-maintained S7-400 can recover from a battery failure without any intervention, provided the EPROM was kept up to date. If load memory is lost or empty: on the S7-400, loss of the RAM load memory occurs when the battery fails during a power outage and no EPROM card is fitted. The program is then gone and must be re-downloaded or restored from a backup file. This scenario, more than any other, justifies the habit of downloading to EPROM after every commissioning change.   3. Work Memory: The Execution Space   Work memory is the integrated RAM in which the CPU executes the program. It is divided internally into a code area and a data area. At download time, the CPU copies the executable blocks from load memory into work memory; at runtime, the CPU fetches instructions and data exclusively from work memory. Work memory is always volatile. On both families it is rebuilt from load memory at every power-on, so a program that "survives" a power cycle does so because load memory survived, not because work memory did. Work memory is the layer that determines whether a program fits. A large data block, a long OB, or a heavily nested FB can exhaust work memory even when the load memory still has free space. When this happens, the download is rejected with a message such as "No user memory available," and the remedy is either to reduce the program size or to move to a CPU with more work memory. Work memory cannot be expanded by adding cards; it is a fixed property of the CPU module itself. This is why the work memory figure in the CPU technical data is the single most important number to check when a project outgrows its controller. If work memory is lost or empty: the CPU stops or fails to start. Because work memory is rebuilt at every power-on, its loss is normally transient and invisible: the CPU simply reloads from load memory. The loss becomes permanent only when load memory is also lost, which is the S7-400 battery scenario described above.   4. System Memory and the Address Areas   System memory is the collective term for the addressable data areas that the instruction set operates on. These areas are implemented in the CPU's internal circuitry, not on any removable medium, and their sizes are fixed properties of each CPU model. Table 2 lists the areas and their roles. Table 2: System memory address areas Area | Symbol | Contents | Notes Process image of inputs | I | Input states copied from the I/O modules at the start of each OB 1 scan | Byte and bit addressing, for example I0.0 through I0.7 in input byte IB0; default range 128 bytes, configurable up to a CPU-specific maximum (2048 bytes on most S7-300 CPUs) Process image of outputs | Q | Output states written to the I/O modules at the end of each OB 1 scan | Byte and bit addressing, for example Q0.0 through Q0.7 in output byte QB0 Peripheral I/O | PI, PQ | Direct access to I/O modules that bypasses the process image | Used for high-speed or time-critical I/O; addressed as PIW/PQW words Bit memory | M | Flags for intermediate logic states | Byte and bit addressing, for example M0.0 through M0.7 in flag byte MB0; size depends on the CPU; on some CPUs the first 256 bytes are reserved for system data and cannot be used freely Data blocks | DB | Structured data storage for the user program | The Retain attribute controls whether DB contents survive a restart Timers | T | S5 timer functions | Number of timers depends on the CPU Counters | C | Counter functions | Number of counters depends on the CPU Local data | L | Temporary variables of the currently active OB, FB, or FC call | Stack-based; depth is limited per priority class   4.1 The process image   The I and Q areas are refreshed through the process image. At the start of the cyclic program, the CPU copies the states of the input modules into the I area; during the cycle, the program reads these consistent snapshots; at the end of the cycle, the CPU copies the Q area to the output modules. This mechanism guarantees that all program sections see the same input states within one scan. Direct peripheral access (PIW, PQW) bypasses the image and reads or writes the module directly, which is faster but not consistent within the scan. A process image that is too small for the installed I/O can be enlarged in the CPU properties in STEP 7, up to the CPU-specific maximum.   4.2 Bit memory M and the flag byte   Bit memory, historically called flags, is the scratchpad of the program. A single flag bit, for example M0.0, holds one Boolean state; eight consecutive bits form flag byte MB0, addressed as M0.0 through M0.7. Flag words (MW) and flag double words (MD) are formed by grouping bytes. The size of the M area differs per CPU: a CPU 314 provides 256 bytes, a CPU 315-2 DP provides 2048 bytes, and a CPU 319-3 PN/DP provides 8192 bytes. On several S7-300 CPUs, part of the M area, for example the first 256 bytes, is reserved for system data used by the operating system and by system functions; using these addresses in the user program can produce erratic behavior, so the technical data of the specific CPU must be consulted before the M area is allocated freely.   4.3 Timers, counters, and local data   Timers (T) and counters (C) are functional elements with an internal state: a timer stores the remaining time, a counter stores the count value. Their numbers are fixed per CPU, for example 256 timers and 256 counters on a CPU 314 and 2048 of each on a CPU 319-3 PN/DP. Local data (L) is the stack area that holds the temporary variables of the currently active call. Every time an FB or FC is called, the CPU reserves a slice of the local data stack for that block's temporaries; deep nesting or large temporary structures can exhaust the stack, which produces a programming error and, if unhandled, a STOP. On S7-300 CPUs the local data stack is typically 32 KB shared across the priority classes; on S7-400 CPUs the capacity is larger and, on newer models, allocated per priority class. If system memory is lost or reset: non-retentive I, Q, M, T, C, and L areas are initialized at every restart, and non-retain DBs are reset to their load values. Retentive areas are restored from load memory, which is the mechanism examined in the next sections.   5. The S7-300 in Practice: MMC, Retentive Data, and the Battery Question   The defining property of the S7-300 memory concept is the absence of a battery. The program lives on the MMC, work memory is reloaded from the MMC at every power-on, and retentive data is stored on the MMC as well. When the CPU detects a power-down, it saves the current values of the configured retentive areas to the MMC; at the next power-up, it restores them. This design has three practical consequences. First, the MMC is a wear item in a narrow sense. Flash memory has a finite erase/write endurance, and every power-down writes the retentive areas. Under normal cyclic operation this is not a concern, but programs that modify retentive data in fast cycles, or that use the system functions SFC 82 to SFC 84 to write data blocks on the MMC in a loop, shorten the card's life. The rated number of write cycles is given in the Siemens documentation for the card. Second, retentive configuration is explicit. In STEP 7, the CPU properties dialog (Hardware Configuration, Retentive Memory tab) defines how many bytes of M, how many timers, and how many counters are retentive. The default retentive flag range on most S7-300 CPUs is M 0.0 through M 15.7. Data blocks are made retentive individually by marking them with the Retain attribute in the block properties. Only the configured ranges survive a power cycle; everything else is initialized. Third, the download behavior is simple and uniform. A normal download in STEP 7 writes the block to the MMC (load memory) and copies it into work memory. There is no separate "download to RAM only" path on the S7-300: with an MMC fitted, every download is automatically non-volatile. The upload direction works the same way: an upload reads from the MMC. Replacement MMC cards in all capacities are listed in the Siemens PLC spare parts catalog, which matters for plants that must keep a programmed spare card on the shelf. The battery question, which dominates S7-400 discussions, simply does not arise on the S7-300. If an S7-300 CPU has no battery, the program cannot be lost to a battery failure. The realistic failure modes are a missing, full, write-protected, or defective MMC, and each of them is examined in Section 9.   6. The S7-400 in Practice: Batteries, EPROM, and the Startup Chain   The S7-400 memory concept is organized around battery-backed RAM, with the Flash EPROM as the safety net. The backup battery, for example 6ES7971-0BA00, maintains the RAM-based load memory and the retentive data while the controller is powered off. The CPU module also carries an integrated rechargeable buffer battery, which maintains the RAM for a limited time, on the order of tens of minutes when fully charged, during a main battery change. This buffer is the reason a battery can be swapped with the power off at all, but it must never be relied on for longer than the manual specifies. The Flash EPROM card, for example 6ES7952-1KM00-0AA0, is the non-volatile layer of the S7-400. It is not required for operation, but it is the difference between a recoverable and a catastrophic battery failure. The card family spans from 64 KB up to 64 MB, and the maximum size depends on the CPU. The startup chain described in Section 2.2 means that a CPU with a current EPROM card recovers automatically from a flat battery; a CPU without one starts into STOP and needs a re-download. Download behavior on the S7-400 has two levels, and confusing them is a common source of field problems: 1. A normal download writes the block to the RAM load memory and to work memory. The change is active immediately but is volatile: it survives a power cycle only while the battery keeps the RAM alive. 2. "Download to EPROM" (or "Copy RAM to ROM") writes the current load memory contents to the Flash EPROM card. The change then survives even a total battery loss. The classic S7-400 failure sequence is therefore: download a modification in the afternoon, never copy RAM to ROM, and find two weeks later, after a power outage with a flat battery, that the CPU restarts with the old program from the EPROM. The modification existed only in RAM and was lost. Keeping the EPROM current after every commissioning change is the single most effective memory-related maintenance rule for the S7-400. The S7-400 reports its battery state continuously. A battery-low condition lights the BATF LED on the front of the CPU or power supply and writes an entry to the diagnostics buffer. STEP 7 shows the detailed state in Hardware Diagnostics / Module Information on the Battery tab, which lists the battery status and, on many CPUs, the estimated remaining backup capacity. Backup batteries such as the 6ES7971-0BA00 are stocked in the PLC spare parts range precisely because they are a consumable with a service life measured in years, not decades.   7. Memory Sizing Reality per CPU   The practical question in every memory-related project discussion is the same: how much work memory and how much load memory does the CPU actually have? Table 3 gives representative figures for five widely installed CPUs. The work memory figure is fixed; the load memory figure is the maximum size of the MMC or EPROM card the CPU accepts. Table 3: Representative CPUs and their memory CPU | Order number | Work memory | Load memory (max) | Typical use CPU 314 | 6ES7314-1AG14-0AB0 | 128 KB | MMC up to 8 MB | Medium machines, standard S7-300 applications CPU 315-2 DP | 6ES7315-2EH14-0AB0 | 256 KB | MMC up to 8 MB | Distributed I/O via PROFIBUS DP CPU 319-3 PN/DP | 6ES7318-3EL01-0AB0 | 2 MB | MMC up to 8 MB | Large S7-300 applications with PROFINET CPU 414-2 | 6ES7414-2XK05-0AB0 | 512 KB | RAM plus EPROM up to 64 MB | Mid-range S7-400 applications CPU 417-4 | 6ES7417-4XT05-0AB0 | 4 MB | RAM plus EPROM up to 64 MB | High-performance S7-400 applications Two sizing rules follow from the table. First, work memory is the binding constraint for program logic. A project with large data blocks or many blocks in the cyclic path needs work memory headroom, because the CPU executes from work memory and cannot page code in from load memory on demand. Second, load memory is the binding constraint for project data: symbols, comments, and technology objects are stored only in load memory. A project that compiles to 300 KB of code may still need a 2 MB MMC once comments and symbol information are included. The general practice is to size the MMC generously at commissioning, because a card swap later requires a full download and a brief production stop.   8. Configuring Retentive Data   Retentive data is the state that must survive a power cycle: finished-part counters, recipe selections, mode flags, and accumulated totals. The configuration procedure is identical in structure on both families, with the storage mechanism differing underneath. On the S7-300, open the CPU properties in Hardware Configuration and select the Retentive Memory tab. There, define the retentive ranges for bit memory (for example 16 bytes of M by default), the number of retentive timers, and the number of retentive counters. Data blocks are handled individually: in the DB properties, mark the block as Retain. Retentive data is then stored on the MMC at power-down and restored at power-up, which is why it survives without any battery. On the S7-400, the same dialog defines the retentive ranges, but the storage mechanism is the battery-backed RAM. Retentive values survive a power cycle as long as the battery is healthy. If the battery fails while the controller is powered off, retentive data is lost and the affected DBs are reinitialized to their load values at the next startup. This is why the battery state of an S7-400 is a maintenance topic, not an operational detail. Three configuration errors account for most retentive-data complaints. The retentive range is not configured at all, so flags reset at every restart. The range is configured but the DB lacks the Retain attribute, so DB contents reset even though M flags survive. Or the range is configured on the wrong CPU in a multi-CPU project, so the intended CPU resets while an unused one retains. All three are diagnosed in minutes by comparing the Retentive Memory tab with the observed behavior after a test power cycle.   9. Failure Modes and Diagnostics   Memory faults on the S7-300/400 present themselves through the LEDs, the diagnostics buffer, and the behavior of downloads and uploads. Table 4 collects the common failure modes, their causes, and the diagnostic path for each. Table 4: Memory-related failure modes and diagnostics Symptom | Likely cause | Diagnostic path | Remedy CPU in STOP; SF and STOP LEDs lit; diagnostics entry "STOP due to memory error" | MMC missing or defective (S7-300), or load memory corrupt | Read the diagnostics buffer via STEP 7 (accessible nodes, module information); check the MMC seating | Insert a known-good MMC with a backup of the program; re-download; replace the card if defective Download rejected with "No user memory available" | Work memory or load memory capacity exhausted | Compare project block sizes with the CPU work memory; check free load memory | Delete unused blocks; reduce DB sizes; move to a CPU with more work memory or a larger MMC Download rejected with "memory card is write-protected" | MMC slider in locked position | Inspect the slider on the card housing | Open the slider; repeat the download Download rejected on an S7-300 with no card inserted | MMC absent | Check the card slot; read the diagnostics buffer | Insert the MMC; the CPU then accepts the download S7-400 BATF LED lit; diagnostics entry "battery low" | Backup battery exhausted or missing | Module Information, Battery tab; check voltage and status | Replace the battery per the procedure in Section 11; verify RAM contents afterward S7-400 restarts with an older program after a power outage | Battery flat and EPROM card holds an older version than the last RAM download | Compare the EPROM date with the last commissioning change | Copy RAM to ROM / download to EPROM after every change; replace the battery Upload returns no blocks or an incomplete project | Blocks exist only in work memory, or the MMC holds an older version (S7-300) | Attempt upload from the CPU; check which blocks are listed | Download the current program to the MMC first; then upload Retentive data lost after a restart | Retentive ranges not configured, DB without Retain attribute, or MMC removed at power-down (S7-300) | Review the Retentive Memory tab; perform a controlled test power cycle | Configure the retentive ranges and Retain attributes; re-download SFC 82/83/84 call reports "No user memory available" | MMC full or write cycle limit reached during runtime data logging | Check free MMC space; review the call parameters | Free space on the card; archive and delete old logged data blocks Two general rules make these diagnostics faster. First, the diagnostics buffer is the primary evidence: it records the stop cause, the time stamp, and the module that triggered the event, and it is readable even from a CPU in STOP. Second, the distinction between load memory and work memory explains most upload/download surprises: if a block is not in load memory, it cannot be uploaded; if it is not in work memory, it cannot be executed.   10. Maintenance and Backup Practice   Memory maintenance on legacy S7-300/400 equipment follows a small set of rules that prevent nearly every failure mode in Table 4. Back up before you touch. A full upload of the program and the Hardware Configuration to the engineering station should precede any download, any memory card operation, and any battery work. The backup file is the insurance that makes every subsequent step reversible. Many plants schedule a fresh backup after every commissioning change and keep the file on a server with the date in the file name. Check the S7-400 battery on a schedule. The battery state is visible in STEP 7 Hardware Diagnostics / Module Information on the Battery tab, and the BATF LED gives a local indication. A monthly check of the BATF LED during routine rounds, plus a quarterly review of the Battery tab, catches a weak battery long before it becomes a production event. Battery service life is measured in years, but it varies with ambient temperature and the duration of power outages, so calendar-based replacement is less reliable than status-based replacement. Handle MMCs by the book. The MMC may be inserted or removed only with the CPU powered off. Removing a card during operation, or during a download, can corrupt the card and forces a format and a full re-download. Cards should be stored in anti-static packaging, labeled with the project name and firmware version, and write-protected with the slider once the content is final. A programmed spare card on the shelf is the fastest disaster recovery an S7-300 plant can have; the Siemens PLC spare parts range covers the card family from 512 KB to 8 MB. Think about the power supply. The S7-300 is fed by the PS 307 and the S7-400 by the PS 407, both available for 120 V/60 Hz and 230 V/50 Hz mains; the input range is printed on the type plate of each module. The modules carry CE marking for the European market and UL/CSA listings for North American installations. A failing power supply produces memory symptoms before it produces a total failure, because brown-outs corrupt RAM contents and trigger restart sequences. Voltage measurements at the load terminals belong in the same maintenance round as the battery check. Stock spares for legacy plants. Plants running S7-300/400 hardware beyond its original service life should hold, at minimum, one programmed MMC per CPU type, one spare backup battery per S7-400, and one spare CPU of each type in use. Older CPUs are increasingly difficult to source, so the spare CPU should be procured while the type is still available. If the plant uses Flash EPROM cards, a spare card with the current program completes the set. The cost of a programmed card and a battery is small compared with the cost of an unplanned production stop, and prices in USD vary with region and availability.   11. Frequently Asked Questions   Does the S7-300 lose its program when the battery dies? No, because the S7-300 has no battery for program storage. The program resides on the MMC, and work memory is reloaded from the MMC at every power-on. A discharged battery is therefore not a cause of program loss on the S7-300; most S7-300 CPUs do not even have a battery compartment. The battery question applies to the S7-400, where the RAM-based load memory depends on the backup battery while the controller is powered off. What happens if the MMC is removed while the CPU is running? The CPU can go to STOP, and the card itself can be damaged, because the CPU writes to the MMC at power-down and during downloads. Siemens specifies that the MMC may be inserted or removed only with the power off. If a card was removed while running, power the CPU down, reinsert the card, and check the diagnostics buffer. If the card was corrupted, format it and re-download the program from the backup. How do I make data retentive on an S7-300? Open the CPU properties in Hardware Configuration and select the Retentive Memory tab. Define the retentive ranges for bit memory (default M 0.0 to M 15.7), the number of timers, and the number of counters. For data blocks, mark the block with the Retain attribute in its properties. The retentive data is then saved to the MMC at power-down and restored at power-up, without any battery. Note that only the configured ranges retain their values; everything else is initialized at restart. What is the S7-400 battery change procedure? First, confirm that the current program is stored on a Flash EPROM card or in a backup file on the engineering station; this step is mandatory. Then, with the CPU powered on, open the battery compartment and replace the cell with a new one of the same type (6ES7971-0BA00), working within the buffer time provided by the integrated rechargeable battery, typically on the order of tens of minutes when fully charged. After insertion, confirm that the BATF LED extinguishes and verify the status in Module Information on the Battery tab. If the CPU was powered off and the RAM was lost, restore the program from the EPROM or from the backup before restarting production. Can I download to work memory only? On the S7-300, no: with an MMC fitted, every download writes to the MMC and copies into work memory, so every download is automatically non-volatile. On the S7-400, a normal download writes to the RAM load memory and to work memory; the change is volatile unless you then download to the EPROM or copy RAM to ROM. A change that exists only in RAM survives a power cycle only while the battery keeps the RAM alive. If the battery fails during an outage, the change is lost and the CPU restarts with the EPROM version. Why does my upload show no blocks? An upload reads from load memory. On the S7-300, blocks that exist only in work memory cannot be uploaded, which typically happens when the MMC was replaced or formatted after the last download. Download the current program to the MMC first, then perform the upload. On the S7-400, verify that the RAM load memory, not only work memory, contains the program; if the CPU was restarted from the EPROM after a battery loss, the upload returns the EPROM version. How long does the S7-400 battery last, and when should it be replaced? The service life depends on the battery chemistry, the ambient temperature, and the frequency and duration of power outages. The reliable method is status-based replacement: replace the cell when the BATF LED lights or when Module Information reports a low state. In a powered-up rack, several years of service are typical. The rechargeable buffer battery on the CPU gives a limited window for a main battery change, so a replacement cell should be on hand before the procedure starts.   12. Summary   The S7-300/400 memory concept is a three-layer model. Load memory holds the complete program and is non-volatile (MMC on the S7-300, battery-backed RAM with optional Flash EPROM on the S7-400). Work memory is the volatile integrated RAM from which the CPU executes, and it is rebuilt from load memory at every startup. System memory provides the address areas I, Q, M, T, C, L, and DB, with retentive subsets configured in STEP 7 and restored from load memory at restart. Most field problems reduce to a small number of causes: a missing or write-protected MMC on the S7-300, a flat battery or an outdated EPROM on the S7-400, a retentive range that was never configured, or a program that exceeds work memory. Each has a defined diagnostic path through the LEDs, the diagnostics buffer, and Module Information, and each has a defined remedy. The maintenance rules that prevent them are equally few: back up before any download, keep the EPROM current on the S7-400, check the battery on a schedule, handle MMCs only with the power off, and keep a programmed spare card and a spare battery on the shelf. For plants that run legacy S7-300/400 hardware, these rules are not optional diligence; they are the difference between a brief intervention and a full re-commissioning.   13. Maintenance Checklist   · [ ] Full program and Hardware Configuration backed up to the engineering station after every commissioning change · [ ] MMC inserted in every S7-300 CPU; spare programmed MMC stored per CPU type (write-protect slider closed) · [ ] MMC slider position verified before downloads; cards inserted and removed only with power off · [ ] S7-400 BATF LEDs checked during routine rounds (monthly) · [ ] S7-400 battery status reviewed in Module Information, Battery tab (quarterly); replacement battery in stock · [ ] Flash EPROM cards up to date after every download (Copy RAM to ROM / download to EPROM) · [ ] Retentive ranges and Retain attributes verified against the process requirements after any configuration change · [ ] Retentive behavior confirmed with a controlled test power cycle after commissioning · [ ] Diagnostics buffer reviewed periodically; unexplained entries investigated before they become stops · [ ] Spare CPUs, MMC cards, batteries, and EPROM cards stocked for each CPU type in service · [ ] PS 307 / PS 407 input voltage (120 V/60 Hz or 230 V/50 Hz) and output voltage verified at the load terminals URL Slug: siemens-s7-300-400-memory-concept --------------------------------------------------------------------------------------------- 🏢 About TZ Tech   TZ Tech is a leading supplier of industrial automation, electrical, instrumentation, and telecommunications components. We specialize in sourcing ready-to-ship distributor stock, allowing us to offer highly competitive pricing and short lead times. Thanks to our extensive inventory, we can even source rare and discontinued parts that are hard to find elsewhere.   🛡️ Our Quality Commitment  We understand that quality is your top priority. Every component undergoes a strict screening and inspection process so you can buy with absolute confidence. For legacy or discontinued parts, we believe in complete transparency and will always provide an honest, accurate report on the product's condition. Plus, all brand-new parts come backed by a full 1-year warranty.  ✉️ Get in Touch Have a project or a part you need? Send us your inquiry today! Our team is dedicated to providing a fast response within 6 hours (excluding weekends).
  • Siemens S7-300: Maintenance, Troubleshooting & Manuals Guide
    Siemens S7-300: Maintenance, Troubleshooting & Manuals Guide Jun 18, 2026
    The 3 AM Phone Call   The line went down at 2:47 AM. A Siemens S7-300 CPU on a bottling line had faulted with an LED pattern no one on the night shift had seen before — SF red, BF flashing, and the CPU in STOP mode. The plant electrician cycled power, no change. Swapped the memory card from a spare unit, no change. Three hours of lost production later, someone finally checked the backup battery voltage: 1.8 V. Dead battery on a CPU315-2 DP (6ES7 315-2AG10-0AB0) had corrupted the RAM-based user program. No backup file existed on the maintenance laptop. That scenario plays out in hundreds of factories every year, and almost all of it is preventable with basic Siemens S7-300 troubleshooting and maintenance.   The S7-300: Why It's Still Running Production Lines   Siemens launched the SIMATIC S7-300 family in the mid-1990s, and despite being officially designated for phase-out, these PLCs are still the backbone of manufacturing lines worldwide. The S7-300 sits between the micro-class S7-200 and the rack-based S7-400 — a modular mid-range controller capable of handling discrete manufacturing, process control, and motion applications. What makes the S7-300 stubbornly persistent is its installed base. A company that spent $50,000 on I/O modules, backplanes, and engineering in 2005 isn't going to forklift-upgrade a working line just because Siemens stopped actively selling the platform. Many S7-300 systems from the late 1990s and early 2000s are still running daily production, held together by knowledgeable maintenance teams and a healthy aftermarket parts supply. The most common CPU models still in service include the CPU315-2 DP (6ES7 315-2AG10-0AB0), the CPU314, and the CPU317-2 PN/DP for lines that need Profinet connectivity. Power comes from the PS307 (6ES7 307-1EA00-0AA0) series, and analog inputs are typically handled by the 8-channel SM331 module (6ES7 331-7KF02-0AB0). These specific model numbers matter because replacement parts, memory cards, and battery types all track back to them. For maintenance teams, the S7-300 presents a unique challenge: the hardware is aging, original documentation can be hard to find, and the engineering software (STEP 7) runs on operating systems that IT departments would rather not support. Knowing where to find a *siemens s7 300 manual* or a *siemens s7 300 manual pdf* before a breakdown happens is the difference between a 20-minute repair and a 20-hour ordeal.   Common Failure Modes in the Real World   Power Supply Issues — PS307 (6ES7 307-1EA00-0AA0)   The PS307 is the most commonly replaced component on an S7-300 rack. These switch-mode supplies fail with age — dried-out electrolytic capacitors, failing fans (on the 10 A version), and intermittent output under load. The warning signs are intermittent system resets, random SF LEDs on multiple modules, or a CPU that boots into STOP mode but runs fine after a power cycle. Test the PS307 with a multimeter at the output terminals. The 24 V DC versions should deliver between 24.0 V and 28.8 V under load. Anything below 22 V and the CPU will drop into STOP mode or behave erratically. If the supply passes voltage tests but you're still seeing intermittent failures, swap it. They're inexpensive relative to the downtime they cause.   CPU Faults — CPU315-2 DP (6ES7 315-2AG10-0AB0)   The CPU315-2 DP is a workhorse, but it has failure patterns worth knowing. The most common is a corrupted user program caused by a dead backup battery (6ES7 971-0BA00). When the battery voltage drops below approximately 2.5 V, the RAM-based program loses integrity. On the next power-up, the CPU goes to STOP with SF red and no amount of cycling will bring it back. The fix is reloading the program via MPI or Profibus from STEP 7 — assuming someone saved a backup. If no backup exists, you're looking at reverse-engineering logic from a working sister machine or paying for a full re-commission. Other CPU failure modes include Profibus communication faults (BF LED flashing or solid red), which are usually wiring or connector issues at the Profibus DP plug rather than the CPU itself. Try swapping the bus connector before replacing the CPU.   Memory Card Failures   The S7-300 uses MMC (MultiMediaCard) format memory cards for program storage. These cards have a limited write-cycle life, and cards from the early 2000s are now reaching end-of-life. Symptoms include the CPU failing to load the program from the card, CRC errors during boot, or the card being recognized in one CPU but not another. The original Siemens MMCs are discontinued and expensive on the secondary market. Third-party equivalents exist, but reliability is inconsistent. A better strategy is to maintain working backups on a laptop and use the memory card slot as a boot medium, not primary program storage.   I/O Module Faults — SM331 (6ES7 331-7KF02-0AB0)   Analog modules are the most sensitive to electrical noise and wiring errors. The SM331 8-channel AI module frequently fails when field wiring shorts 24 V to a signal input channel. Channel diagnostics LEDs (if equipped) or the SF group fault LED will light up. The fix is usually replacing the module, but always check the wiring first. A quick continuity test between each signal wire and ground will catch the 90% case. For more detailed *plc siemens s7 300 troubleshooting* approaches, the PLC section on tztechio.com has compatibility data and spare parts cross-references that save hours of manual research.     Deep Dive: Software, Batteries, Firmware, and Backups   STEP 7 Software Compatibility   The S7-300 programs are engineered using Siemens STEP 7. The critical compatibility table: STEP 7 Version | Supports | Windows STEP 7 V5.4 | S7-300 all CPUs | XP, Vista STEP 7 V5.5 | S7-300 all CPUs | Win7 (32/64) STEP 7 V5.6 | S7-300 all CPUs | Win7, Win10 (64-bit) TIA Portal V13+ | S7-300 (limited) | Win7, Win10 The original STEP 7 Classic (V5.x) is the safest choice for S7-300 work because TIA Portal's support for S7-300 is limited and certain older CPU firmware versions are not fully compatible. TIA Portal V13 through V17 can handle S7-300 CPUs with firmware V3.x and above, but if you're supporting a machine from 2003 running firmware V2.x, you need STEP 7 Classic. Finding a working *siemens step 7 300 manual* or a *siemens s7 300 manual programming* PDF is essential for anyone maintaining these systems. The official Siemens support portal still hosts many of these documents, but the search filters can be tricky. Use the exact model number as the search term for best results.   Battery Replacement — 6ES7 971-0BA00   The S7-300 backup battery (6ES7 971-0BA00) is a 3.6 V lithium cell that maintains the user program in RAM when the main power is off. Siemens recommends replacement every 3-4 years. In practice, most plants ignore this until the CPU loses its program. Replacement procedure: 1. Put the CPU in STOP mode. 2. Note the battery indicator — the yellow BATF LED means low battery. 3. Open the battery compartment door on the front of the CPU. 4. Remove the old battery (observe polarity). 5. Insert the new battery — 6ES7 971-0BA00 or any compatible 3.6 V lithium cell with the correct connector. 6. Power cycle the system to verify the program loads correctly. 7. Document the replacement date on the cabinet door. The battery only maintains the RAM when the PLC is powered off. If the system stays powered on continuously, a dead battery causes no problems until the next planned or unplanned shutdown. Always replace the battery during a scheduled outage — never hot-swap it on a running line unless you have a verified backup file.   Firmware Updates   S7-300 CPUs rarely need firmware updates unless you're adding new hardware modules or resolving a specific bug. Firmware files are available from the Siemens Industry Online Support portal. The update process uses a memory card: 8. Download the firmware update file (a .UPD file for S7-300). 9. Copy it to an MMC card. 10. Insert the card in the CPU while it's powered on. 11. The CPU detects the firmware file and prompts an update. 12. Confirm, wait for completion (CPU restarts automatically). Firmware updates wipe the user program. Always back up the program before updating firmware.   Backup Procedures   A proper S7-300 backup strategy has three layers: · Layer 1: Full program upload from CPU to STEP 7 (File > Upload Station to PG). Save the entire project. · Layer 2: An MMC card with the current program, stored in a static-safe bag inside the cabinet. · Layer 3: An offline archive of the STEP 7 project (zipped or saved to a network share). Label every backup with the machine name, date, and CPU firmware version. The worst time to discover that a backup is from 2017 is when your CPU fails in 2025.   Pricing & Availability of S7-300 Spare Parts   Siemens officially discontinued the S7-300 family for new sales, though support continues for existing installations. This means new-old-stock (NOS) genuine Siemens parts command premium prices: Component | Typical Price Range (Second Market) CPU315-2 DP (6ES7 315-2AG10-0AB0) | $400 – $1,200 PS307 5A (6ES7 307-1EA00-0AA0) | $100 – $300 SM331 AI 8x12bit (6ES7 331-7KF02-0AB0) | $200 – $600 Backup Battery (6ES7 971-0BA00) | $15 – $40 MMC 64KB | $30 – $100 Used and refurbished parts are available from industrial surplus dealers, eBay Industrial, and specialized PLC distributors. Quality varies significantly. A refurbished unit from a reputable supplier that tests under load is worth the 20-30% premium over untested "as-is" surplus. Budget-conscious plants should identify the top 5 most failure-prone modules on each S7-300 system and keep spares on the shelf. For most lines, that means one spare PS307, one spare CPU, one spare of each I/O module type, and two spare batteries. The inventory cost is usually under $2,000 per line and pays for itself the first time a module fails at 3 AM. Frequently Asked Questions   Q: Can I program an S7-300 without STEP 7? A: No. The S7-300 requires Siemens STEP 7 (Classic V5.x or TIA Portal) for programming, configuration, and diagnostics. Open-source alternatives like OpenPLC do not support S7-300 hardware. Q: What does the red SF LED on my CPU315-2 DP mean? A: The SF (System Fault) LED indicates a hardware fault, a programming error, or a communication problem. Connect STEP 7 and check the diagnostic buffer (PLC > Module Status > Diagnostic Buffer). The buffer shows the exact error with a timestamp. Q: How long does the S7-300 backup battery last? A: Siemens rates the 6ES7 971-0BA00 battery for 3-4 years in storage or unpowered PLC. In practice, if the PLC is powered on continuously, the battery lasts its full shelf life (about 5 years from manufacture date). Replace it every 3 years during planned maintenance. Q: My S7-300 CPU won't boot after a power outage. The SF LED is solid red. What now? A: 90% chance it's a corrupt program from a dead backup battery. Replace the battery, then reload the program from STEP 7 or an MMC card. If the memory card has the program, insert it and power cycle. The CPU should copy the program from the MMC to RAM. Q: Is the S7-300 still supported by Siemens? A: Siemens announced the phase-out of the S7-300 family, but the product is not fully discontinued for support. The Siemens Industry Online Support portal still provides manuals (including *siemens s7 300 manual* and *siemens simatic s7 300 manual* PDFs), firmware updates, and technical support for existing installations. Q: Can I replace an S7-300 with a newer Siemens PLC without rewiring? A: Direct drop-in replacement is not possible. The S7-1200 and S7-1500 families use different form factors, backplane connections, and engineering software (TIA Portal only). Replacement requires a new panel layout, rewiring, and program migration. Budget at least 40 engineering hours per CPU for a full migration. Q: What's the cheapest way to get a *siemens s7-300 pdf* manual? A: All official S7-300 manuals are free from the Siemens Industry Online Support portal (support.industry.siemens.com). Search by exact model number (e.g., "6ES7 315-2AG10-0AB0 manual") for the most relevant results. Third-party document aggregation sites often charge for the same PDFs that Siemens hosts for free. Q: How do I know if my SM331 analog module is faulty? A: Check the SF group fault LED. Then disconnect all field wiring and supply a known 4-20 mA or 0-10 V signal from a calibrator. If the channel reads correctly, the module is fine and the problem is in the field wiring. If it reads incorrectly or shows no signal, the channel is likely damaged, typically from overvoltage or short-circuit conditions.   Maintenance Checklist Summary   A quarterly S7-300 maintenance pass takes 30 minutes per rack and catches the most common failure modes before they cause downtime: 13. Inspect PS307 output voltage under load (24-28.8 V DC). 14. Check CPU BATF LED — replace battery if yellow. 15. Verify all I/O module SF LEDs are off. 16. Open STEP 7 and read the CPU diagnostic buffer — clear old entries. 17. Verify the MMC card is seated properly. 18. Upload and archive the current program. 19. Document any LED patterns or error messages observed. 20. Check Profibus connectors for tightness and correct termination resistors. Most S7-300 failures are not sudden. They announce themselves through intermittent faults, borderline power supply voltages, or LEDs that maintenance crews tuned out months ago. A disciplined approach to monitoring, documentation, and spare parts inventory turns the S7-300 from a reliability risk into a known quantity — one that keeps running until the plant decides it's time to modernize.
Subscribe

Please read on, stay posted, subscribe, and we welcome you to tell us what you think.

submit
Copyright 2026 @ TZ TECH Co., LTD. .All Rights Reserved Disclaimer: We are not an authorized distributor or distributor of the product manufacturer of this website, The product may have older date codes or be an older series than that available direct from the factory or authorized dealers. Because our company is not an authorized distributor of this product, the Original Manufacturer’s warranty does not apply.While many DCS PLC products will have firmware already installed, Our company makes no representation as to whether a DSC PLC product will or will not have firmware and, if it does have firmware, whether the firmware is the revision level that you need for your application. Our company also makes no representations as to your ability or right to download or otherwise obtain firmware for the product from our company, its distributors, or any other source. Our company also makes no representations as to your right to install any such firmware on the product. Our company will not obtain or supply firmware on your behalf. It is your obligation to comply with the terms of any End-User License Agreement or similar document related to obtaining or installing firmware.

Sitemap | Blog | XML | Privacy Policy

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

Home

Products

whatsApp

contact

YOUR COOKIE SETTINGS

In addition, with your permission, we want to place cookies to make your visit anointeraction with slOC more personal. For this we use analytical and advertisingcookies. With these cookies we and third parties can track and collect yourinternet behawior inside and outside super-instrument.com. With this we and third parties adapt super-instrument.com and advertisementsto your interest. By clicking Accept you agree to this. If you decline, we only usethe necessary cookies and you unfortunately will not receive any personalizedcontent. Please visit our Cookie policy for more information or to change yourconsent in the future.

Accept and continue Decline cookies