PLC ENGINEERING

Allen Bradley

Home

Allen Bradley

  • Studio 5000 and RSLogix 5000 Firmware and Version Management: A Rigorous Guide
    Studio 5000 and RSLogix 5000 Firmware and Version Management: A Rigorous Guide Sep 02, 2026
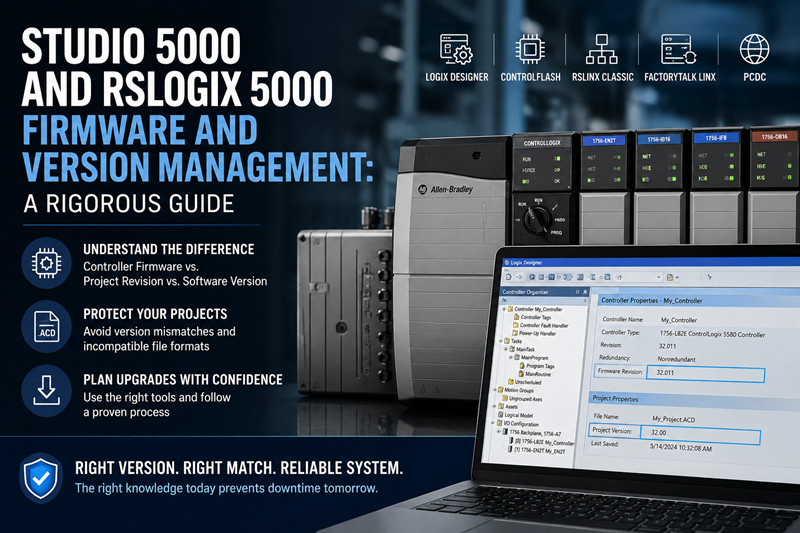
      Firmware is the operating system that runs on the controller. Project revision is the format version of the .ACD file. These two numbers are frequently confused, and the confusion is expensive. A maintenance engineer who mistakes one for the other can convert a healthy project into a file that no installed software can open, or send a running production line through an unplanned firmware download for which no backup exists. Correct terminology follows Rockwell Automation usage: Logix Designer, ControlFLASH, RSLinx Classic, FactoryTalk Linx, and the Product Compatibility and Download Center (PCDC).   1. Definitions   1.1 Controller firmware   Firmware is the executable operating system stored in nonvolatile memory on the controller. For a ControlLogix or CompactLogix controller, the firmware implements the Logix execution engine: it runs the task model, executes the routines, communicates over the backplane and the network, and provides the services that Logix Designer calls during an online session. A controller without firmware is inert. New controllers ship from the factory with firmware already loaded, and the same physical hardware can run different firmware revisions over its service life. Rockwell identifies firmware by a revision number. The revision is the number shown in RSLinx Classic or FactoryTalk Linx when the engineer browses to the controller, and it is the number that must be weighed against the software version on the PC. When this guide says "controller revision," it means that firmware revision number.   1.2 Project revision   A Logix Designer project is a single file with the .ACD extension. The file has its own format version, and that format version is the project revision. When a dialog says "project revision 32," it is describing the file format, not the controller. The project revision is written into the file by the software that created or last saved it. The project revision and the controller revision usually match in a healthy system, because Logix Designer creates a project at the revision of the controller it targets. The match is a convention, not an identity. A project at revision 32 can target a controller at firmware 32, and the two numbers happen to be equal. The confusion begins when an engineer treats the project revision as if it were the controller firmware, or the controller firmware as if it were a file property.   1.3 Software version   The software version is the version of the installed application: RSLogix 5000 for versions 1 through 20, and Studio 5000 Logix Designer for version 21 and later. Rockwell renamed RSLogix 5000 to Studio 5000 Logix Designer starting around version 21, released in 2012. The change was a rebranding and a packaging change, not a new product. The application that opens .ACD files is the same lineage, and the version numbering continued without a break. Version 20 is therefore RSLogix 5000, and version 21 is Studio 5000 Logix Designer. The name matters only near that transition point. An engineer should read "Studio 5000 version 32" and "RSLogix 5000 version 20" as the same kind of quantity. Each software version has a native project revision. Studio 5000 Logix Designer version 32 creates and edits projects at revision 32. The software can open projects at older revisions under conditions described below, and it can create projects for controllers at older firmware revisions under conditions as well. The native pairing is the relationship that matters: software version N pairs with project revision N and controller revision N.   1.4 Module firmware   The controller is not the only device with firmware. Every intelligent module in a Logix system carries its own: the 1756-EN2T Ethernet communication module, the 1756-IB16 and other discrete I/O modules, the 1756-IF8 and other analog modules, the 1756-CNB and 1756-DNB bridges, and the 5069 and 1769 I/O families. Each module has its own firmware revision, and each is updated separately with ControlFLASH. Module firmware matters for two reasons. The project stores the expected firmware revision for every module in the I/O configuration, and Logix Designer compares expectations against reality at online time. Communication modules also sit on the online path to the controller, so a module with incompatible firmware can block the connection before the engineer ever reaches the controller. Module firmware and controller firmware are updated with the same tool, but they are different operations, and an upgrade plan must treat them separately.   2. The compatibility model   The compatibility model has three inputs: the software version, the project revision, and the controller revision. The rules below describe how the three may combine. Once the rules are stated, every dialog and every failure mode becomes readable.   2.1 Project files: no forward compatibility, limited backward compatibility   A project saved by a newer version of the software cannot be opened by an older version. This rule has no exceptions in the Logix product line. If a project was created and saved in Studio 5000 Logix Designer version 33, no installation of version 32 can open it. The older software does not understand the newer file format, and Rockwell does not ship a downgrade converter for project files. Backward compatibility exists and is limited. An older project opens in newer software, and the newer software converts it. The conversion is one-way. After the newer version saves the file, the project revision has advanced, and the older software can no longer open it. A project at revision 20 that is opened in version 33 and saved becomes a revision 33 project. The original revision 20 file is gone unless a copy was kept. This is the first expensive failure mode. An engineer opens an old project to look at a routine, the software prompts to convert, the engineer accepts, saves, and the plant loses the ability to open that project with the old software that still matches the running controllers. The safe practice follows directly from the rule: keep the original file untouched, and convert into a new file name.   2.2 Software version and controller revision: the online requirement   Going online is the operation where software and controller meet directly. Logix Designer establishes a communication path through RSLinx Classic or FactoryTalk Linx, finds the controller, and compares versions. The comparison is strict. To go online with a controller, the software version must be compatible with the controller's firmware revision. The practical expression of the requirement: software at a version equal to or newer than the controller revision can go online. Software older than the controller revision cannot. A controller at revision 32 requires software at version 32 or newer. Version 31 cannot go online with that controller, and no driver setting or compatibility mode changes that fact.   2.3 Upload and download   Upload is the transfer of the project from the controller to the PC. Upload works when the software version is equal to or newer than the controller firmware revision. The software reads the program from the controller, reconstructs a project, and writes the file at the revision of the controller it read. Uploading from a controller at revision 24 with version 32 software therefore produces a project at revision 24, and that file is openable by software at version 24 or newer, including the older software the plant already owns. Uploading with software older than the controller revision is not possible: the older software cannot interpret the data structures of the newer controller. A controller at revision 32 with only version 30 software available cannot be uploaded. The fix is to obtain version 32 software or newer, not to attempt workarounds. Download is the transfer of the project from the PC to the controller. Download requires the project revision to match the controller revision, unless the engineer explicitly changes the controller revision as part of the download. When the revisions differ, Logix Designer offers to change the controller revision before it downloads the project. Changing the controller revision means flashing new firmware into the controller. There is a legitimate way to make the two sides match without a conversion: the New Project dialog in Logix Designer offers a revision list for the selected controller, and that list includes revisions older than the software version. A plant with version 32 software can create a project at revision 24 for a v24 controller, and the file is written at revision 24. This is how an OEM produces a deliverable that an older software version can open, and it is the correct tool when the project revision and the controller revision must be aligned by design. The download path is where the second expensive failure mode lives. The change-controller-revision prompt appears during a routine download, an engineer accepts it without reading it, and the controller receives new firmware. A running machine whose controller was never backed up loses its program if the flash fails partway. Even a successful firmware change can leave I/O connections and module firmware expectations in an inconsistent state, because the new controller revision may expect newer module firmware than the chassis actually runs.   2.4 What the revision mismatch dialogs actually mean   Three dialogs dominate the field reports. The first is the project open error. The software reports that the project was created with a newer version of the software and refuses to open the file. No workaround exists inside the older software. The fix is to obtain the newer software version, or to ask the source of the file for a copy at the plant's revision, which the newer software can produce for projects it can open. The second is the Go Online mismatch. The software finds the controller, sees a revision difference, and offers to change the controller revision. Accepting the offer flashes the controller. The dialog is a request for permission to change firmware, not a notice. The safe response is Cancel, followed by a decision about which side should move: install matching software, or plan a controlled firmware upgrade. The third is the download mismatch with the change-controller-revision option. It is the same operation as the second, reached through a different path. The meaning is identical: the project revision and the controller revision differ, and the software proposes to make them equal by writing new firmware to the controller. The Who-is-online list in Logix Designer shows the engineers currently connected to each controller and the controllers each connection targets. It belongs in this discussion because the Go Online sequence is where an engineer first sees the revision of the target controller, and where an unplanned acceptance of the change-controller-revision offer does its damage. The dialog appears once per online attempt, it is phrased as a routine question, and the cost of accepting it without preparation is an altered or bricked machine. The Go Online flow is also where the engineer sees whether the controller can be reached at all: if the communication path fails before the version comparison, the problem is the driver or the network, and if the comparison fails, the problem is the revision.   2.5 Why the three numbers line up   The alignment of software version, project revision, and controller revision is not accidental. When an engineer creates a new project, Logix Designer asks for the controller catalog number and for the controller revision. The project file is written at the selected revision, and that revision is stored as the target. A healthy machine runs a controller at the revision the project targets, and the project lives at the revision of the software that manages it. Drift in any one of the three numbers produces one of the dialogs above. Online edits add a second kind of drift. An engineer who goes online and edits logic changes the program stored in the controller without changing the .ACD file on the PC. The controller and the file now differ, even though every version number matches. This is why a full upload belongs in any upgrade procedure: the upload captures the actual state of the controller, including edits that were never saved to the file.   2.6 Common situations, read through the model   Four situations recur in support requests, and each one is the compatibility model in action. Situation one: an OEM sends a project file at revision 33, and the plant runs Studio 5000 version 30. The file will not open. The plant either installs version 33, or asks the OEM for a project at revision 30, which the OEM's newer software can create. Neither option changes the controllers, so the plant's existing online capability is unaffected. Situation two: a replacement controller arrives from the warehouse and the plant cannot go online with it. The replacement was flashed to a newer firmware revision than the plant's software supports. The options are to flash the replacement down to a revision the plant's software supports, if that revision exists for the catalog number, or to upgrade the plant's software. Flashing down is a firmware operation with the same risks as any other flash, and it needs the same backup discipline. Situation three: an engineer downloads a project and the software asks to change the controller revision. The engineer accepts, and after the download the I/O tree shows module faults. The controller revision moved, the module firmware did not, and the project's module expectations no longer match the chassis. The fix is a planned module firmware upgrade, which is why the procedure in section 6 treats the whole chassis, not only the controller. Situation four: an engineer cannot upload from a controller that a contractor upgraded during commissioning. The contractor flashed the controller to revision 32 and the plant owns version 30 software. Upload is impossible until the plant obtains version 32 or newer. This situation is common after third-party work, and it is why the controller revision belongs on any handover checklist.   3. Hardware firmware limits   Each controller family has a range of firmware revisions it can run. The figures below are the well-established limits. Rockwell adjusts support policy over time, and the authoritative source for any specific catalog number is the Product Compatibility and Download Center (PCDC). Check the PCDC before planning an upgrade. A firmware revision that does not exist for a given catalog number cannot be selected in ControlFLASH in any case. Controller family | Catalog numbers | Maximum firmware (typical) | Notes ControlLogix 5560 | 1756-L61, 1756-L62, 1756-L63 | approximately v20 | Rockwell ended feature development for the L6x family at that point. The exact supported range depends on the catalog number; check the PCDC. ControlLogix 5570 | 1756-L71 through 1756-L75 | approximately v24 | The L7x family tops out near v24. Check the PCDC for the exact range. ControlLogix 5580 | 1756-L81 through 1756-L85 | v24 and newer | The L8x family requires v24 or newer and will not accept older firmware. ControlLogix 5580, E series | 1756-L81E through 1756-L85E | v28 and newer (general) | The 5580 family generally requires v28 or newer. Check the PCDC for the current maximum. CompactLogix 5370 | 5069-L306ER and related 5069 catalog numbers | v30 and newer (general) | The 5069 family generally requires v30 or newer. Check the PCDC for the current maximum. CompactLogix 5370 | 1769-L16ER through 1769-L37ERM | approximately v20 to v36 | The supported range depends on the model and on Rockwell support policy. Check the PCDC for the exact figure for your catalog number. Three practical consequences follow from the table. First, an L61 at revision 20 cannot be upgraded to revision 24; the hardware does not support it, and no firmware file at revision 24 exists for that catalog number. Second, an L81 cannot run revision 20 firmware; the controller requires revision 24 or newer and will not accept older firmware. Third, the maximum firmware for the 5580 and 5069 families is a moving target: Rockwell publishes new revisions over time, and the current maximum is exactly the kind of figure the PCDC exists to state. When a plant plans a migration from an L6x to an L8x, the firmware jump from approximately v20 to v24 or newer is part of the project scope, along with the software jump from RSLogix 5000 to a newer Studio 5000 version. The same reasoning applies to a migration from a 1769 CompactLogix to a 5069 CompactLogix: the new controller family sets a new firmware floor and a new software floor, and the old project must be converted into a new project at the new revision before it can be downloaded. Hardware that has reached the end of its firmware range is often the same hardware that has become hard to source, which is why Allen-Bradley spare parts for legacy ControlLogix and CompactLogix platforms remain a normal procurement item for plants that cannot migrate yet.   4. Multiple software versions on one PC   Multiple versions of RSLogix 5000 and Studio 5000 Logix Designer can be installed on the same PC. Rockwell designed the installers to coexist, and many engineers do run version 20 and version 32 on one machine. The coexistence is workable, and it is messy. Licensing is the first complication. RSLogix 5000 and Studio 5000 use FactoryTalk Activation, and each software version needs its own activation. An activation that covers version 32 does not automatically cover version 20. A plant that keeps both installed must keep both activations valid, and an expired activation for one version surfaces as an error that looks like a software fault. Windows compatibility is the second complication. The oldest RSLogix 5000 versions predate modern Windows and do not run on Windows 10 or Windows 11. Version 20, for example, was released in the Windows XP and Windows 7 era, and running it on a modern operating system typically requires a virtual machine. The compatibility matrix in the PCDC states the supported operating systems for each software version. The honest summary: the older the software, the older the Windows it needs. Coexistence itself is the third complication. Different versions share services such as RSLinx Classic and FactoryTalk Linx, and version conflicts surface as drivers that disappear, activation errors, and projects that open in the wrong application when file associations point at the last installed version. A version that worked alone can start failing after a second version is installed. The common engineering solution is a dedicated laptop or a virtual machine per version. A plant with controllers at v20 and at v32 keeps one machine with RSLogix 5000 v20 and one with Studio 5000 v32, and does not mix them. The pattern costs hardware and desk space, and it buys certainty. A plant that keeps a v20 machine alive is usually the same plant that keeps PLC spare parts on hand for hardware Rockwell no longer sells. The virtual machine approach has an extra advantage: the VM image itself is a backup, and a corrupted installation is restored by copying the image rather than by reinstalling the software and re-entering activations.   5. Module firmware versus controller firmware   A Logix chassis contains the controller and its modules, and each module runs its own firmware. The project stores the expected firmware revision for every module in the I/O configuration. When Logix Designer goes online, it compares the expected module revisions against the actual revisions in the chassis and reports differences. Module firmware is updated with ControlFLASH, the same tool used for the controller. The operation is per module: select the module in the flash tool, select the target revision, and flash. The 1756-EN2T Ethernet module is the module most often flashed, because its firmware controls the network path and because Rockwell publishes new EN2T revisions to correct communication defects. The practical rule: module firmware upgrades belong in the same maintenance window as controller firmware upgrades, and they are verified with the same discipline. A project that expects EN2T revision 5 on a module that runs revision 3 produces a mismatch at online time, and the mismatch either blocks the connection or degrades it, depending on the module and the size of the difference. Keep module firmware consistent with the project's expectations, and change both sides deliberately, never one side by accident. A controller firmware upgrade that raises the controller beyond the firmware of its communication modules is a common source of module fault and connection failed reports after an otherwise clean upgrade.   6. The safe firmware upgrade procedure   The procedure below is ordered. Every step exists because a skipped step has caused a real failure. Follow the steps in sequence, and do not merge steps. 1. Verify the current state. Open RSLinx Classic or FactoryTalk Linx, browse to the controller, and record the current firmware revision. Record the revision of every module in the chassis as well, from the I/O configuration in the project or from module properties. The record is the baseline for the entire operation, and it is the reference for the post-upgrade verification. 2. Back up the project. Close the project, copy the .ACD file to two separate locations, and record the project revision. Do not convert the project as part of the backup. The backup must be a byte-for-byte copy of the file that matches the running system. 3. Perform a full upload. Go online with the current software, upload the project from the controller, and save the uploaded copy under a separate name. The upload is the second backup, and it is the one that matters if the .ACD file and the controller have drifted apart. Controllers can contain logic that the file does not, because engineers make online edits. The upload captures the actual state. 4. Check the compatibility matrix in the PCDC. Verify three things: the target firmware revision exists for the controller catalog number, the software version planned for the post-upgrade connection supports that firmware revision, and that software version runs on the operating system of the PC that will go online. A failure in any of the three cancels the upgrade until it is resolved. This step also identifies the module firmware revisions that the target controller revision expects, so the module list from step 1 can be checked against it. 5. Confirm the maintenance window. A firmware download interrupts the controller. The controller stops executing the program for the duration of the flash, and I/O connections drop. Confirm that the process can tolerate the interruption, that the operators have been informed, and that the machine is in a safe state. Do not upgrade a running machine outside a maintenance window, and do not upgrade a machine in the middle of a batch. 6. Run ControlFLASH. Launch ControlFLASH, select the controller, select the target revision, and start the flash. Do not interrupt the flash once it starts. A power loss or a communication break during the flash can leave the controller with a corrupt firmware image. The controller may recover through a boot mode, and the recovery is not guaranteed. Wait for the completion message before touching anything. 7. Verify the result. Power-cycle or reset the controller as the flash tool directs. Go online with the planned software version and confirm that the revision shown in Logix Designer matches the target. Check the I/O connections: every module in the I/O tree should show its expected state, and module firmware mismatches surface at this point. Confirm that the program runs: place the controller in Run mode and observe execution, task timestamps, and I/O values. Keep the pre-upgrade backups until the machine has completed a full production cycle on the new firmware. Module firmware upgrades follow the same procedure, with step 6 repeated for each module. The verification in step 7 then checks the module revisions in the I/O tree instead of the controller revision.   7. Firmware upgrade checklist   Condensed checklist for the maintenance planner: · [ ] Baseline recorded: controller revision and module revisions documented · [ ] Project backed up at its current revision, two copies, not converted · [ ] Full upload performed and saved under a separate name · [ ] PCDC checked: target firmware exists for the controller catalog number · [ ] PCDC checked: planned software version supports the target firmware · [ ] PCDC checked: software version supports the PC operating system · [ ] Module firmware expectations checked against the target controller revision · [ ] Maintenance window confirmed with operations · [ ] Machine in a safe state, no active batch · [ ] ControlFLASH run to completion without interruption · [ ] Controller reset or power cycle performed as directed · [ ] Online verified: controller revision matches the target · [ ] I/O connections verified module by module · [ ] Program confirmed running in Run mode · [ ] Pre-upgrade backups retained until one full production cycle completes   8. FAQ   Q1. Can version 30 open a project saved in Studio 5000 version 32? No. A project saved by a newer version cannot be opened by an older version. Version 30 cannot read the revision 32 file format. Obtain version 32 or newer, or ask the source of the file for a copy at revision 30. Q2. What does the controller revision mismatch message mean when I go online? It means the software version and the controller firmware revision are not compatible, and the software offers to change the controller revision, which writes new firmware to the controller. Cancel the offer unless the change is planned, backed up, and scheduled. Q3. Can I upload from a controller whose firmware is newer than my software? No. Upload requires software at a version equal to or newer than the controller revision. Install matching or newer software before the upload. Q4. Is a firmware upgrade reversible? A controller can be flashed back to an older revision if that revision exists for the catalog number. The reversal is itself a firmware operation with the same risks. A converted project is not reversible: once the newer software saves a converted file, no older software can open it. Q5. Can I run version 20 and version 33 on the same PC? In principle, yes. The practical limits are licensing, Windows compatibility, and shared-service conflicts. Version 20 does not run on modern Windows without a virtual machine. Most plants use a dedicated laptop or VM per version. Q6. What is the difference between controller firmware and module firmware? Controller firmware is the operating system of the controller. Module firmware is the operating system of each individual module, such as a 1756-EN2T. Both are updated with ControlFLASH, and both must match what the project expects. Q7. Where do I find the exact maximum firmware for my controller? In the Product Compatibility and Download Center (PCDC) at Rockwell Automation. The PCDC states the available firmware revisions for each catalog number and the compatible software versions. Consult it before every upgrade.   9. The rule that governs every case   The compatibility model reduces to one sentence: the software version, the project revision, and the controller revision must form a consistent set, and every change to one member of the set is a planned operation. A project file that will not open, an online session that will not start, and a download that wants to change controller firmware are all the same underlying condition: the set is inconsistent. The engineer's job is to identify which member is out of line, decide which member should move, and move it with a backup and a maintenance window in place. For plants that run legacy hardware, the set has a fourth member: the hardware itself. A controller whose firmware range has ended is a controller whose spares are scarce, and the planning horizon for a migration starts at the moment the firmware limit is reached. Allen-Bradley spare parts and ControlLogix spare parts keep legacy lines running while the migration is planned, and the version discipline in this guide keeps the software side of the set stable for as long as the hardware runs. The discipline costs little. The alternative costs a production line. URL Slug: studio-5000-firmware-version-management-guide ------------------------------------------------------------------------------------------- 🏢 About TZ Tech   TZ Tech is a leading supplier of industrial automation, electrical, instrumentation, and telecommunications components. We specialize in sourcing ready-to-ship distributor stock, allowing us to offer highly competitive pricing and short lead times. Thanks to our extensive inventory, we can even source rare and discontinued parts that are hard to find elsewhere.   🛡️ Our Quality Commitment   We understand that quality is your top priority. Every component undergoes a strict screening and inspection process so you can buy with absolute confidence. For legacy or discontinued parts, we believe in complete transparency and will always provide an honest, accurate report on the product's condition. Plus, all brand-new parts come backed by a full 1-year warranty.   ✉️ Get in Touch     Have a project or a part you need? Send us your inquiry today! Our team is dedicated to providing a fast response within 6 hours (excluding weekends).
  • Motion Control ( MC )  & Process Control
    Motion Control ( MC ) & Process Control Dec 22, 2023
    What is motion control? Motion control (MC) is a branch of automation, also called electric drag control. Most of its power sources are based on electric motors. In other words, motion control is actually based on electric motors to control changes in physical quantities such as angular displacement, speed, and torque. The application of motion control in the field of robots and CNC machine tools is more complex than that in special-purpose machines because the latter's motion form is simpler and is often called general motion control (GMC). Motion control is widely used in the packaging, printing, textile and assembly industries. Motion control is actually based on electric motors, and the electric motors here refer to servo motors; if only one servo motor is used in a set of stand-alone equipment, in this case it will focus more on the control of the motor, such as position, speed, Torque control; in this example, the control of a single motor is only a part of motion control. Motion control is mainly for products. It can be said to be a motion control system. The system as a whole includes machinery (motors are just spare parts in machinery), electrical, software, etc. It controls and manages the position and speed of mechanical moving parts in real time. , so that it can be transformed into the desired mechanical motion control according to the predetermined control scheme. There are many kinds of motion control systems, but from the basic structure, the hardware of a typical modern motion control system mainly consists of: host computer, motion controller, power drive device, motor, actuator and sensor feedback detection device.   What is automated process control? The principle of automated process control is to use PLC controllers to collect sensor feedback data, and after analyzing and processing these data, adjust, optimize and control various equipment to improve production efficiency. The objects it controls are generally various types of water pumps, fans, electric valves, etc. The entire system generally consists of PLC control cabinet, power distribution cabinet, control program, various sensors, configuration software, monitoring system, etc. Process automation is generally used in environmental protection industries such as sewage and exhaust gas treatment, and energy-saving industries. It intelligently adjusts various load equipment in industrial production to ensure that they operate at their best to achieve energy saving. Mainly used in the field of traditional industrial automation, it is a large system control with many control objects, such as a production line.   Many Available just wait for you, feel free to ask to get better deal!!!Bou LSales SpecialistBou.l@tztechautomation.com+86-175 5077 6091
  • ControlNet Troubleshooting: A Field Procedure That Gets the Net Back
    ControlNet Troubleshooting: A Field Procedure That Gets the Net Back Sep 09, 2026
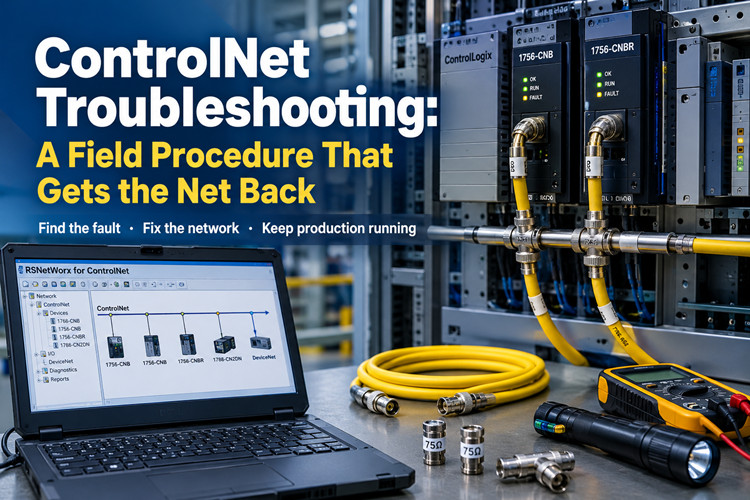
      At 2:17 in the morning the phone wakes you, and the voice on the other end skips the hello. Node 14 dropped and the line is down. Scheduled traffic through the 1756-CNB stopped forty minutes ago, the drives are faulted, and the shift electrician has already reseated every connector he can reach. He wants to know if you are coming. You are coming. Before you get in the truck, take this article with you. Here is the situation you will walk into. A ControlNet trunk built from 1786-RG6 coax, tapped into a row of 1756-CNB and 1756-CNBR modules in ControlLogix racks, a 1788-CN2DN or two carrying I/O down to DeviceNet, and a schedule that RSNetWorx for ControlNet wrote years ago and nobody has backed up since. Rockwell lists ControlNet as Active-Mature, which is a polite way of saying it still supports the product but is not building more of it. The company would rather sell you EtherNet/IP on 1783 switches, and it is right to try. But your plant still runs on coax, and it has to run tomorrow. This is the field procedure that gets the net back. Do the steps in order and do not skip the boring ones, because the boring ones are where these calls usually die.   Tools you need before you start   Round these up before you leave the shop. Every trip back to the truck for a missing part costs twenty minutes of a night that is already long. · RSNetWorx for ControlNet, installed and proven on your laptop. Know which version you carry, and know that the EDS files on that laptop match the devices on the net. A laptop that has not seen the plant in two years will waste your first hour updating itself. · A ControlNet interface for the laptop. The 1784-PCC CardBus card and the 1784-U2CN USB adapter are the two you will meet in the field. Load the driver and configure it in RSLinx before you leave, and test the card against a live net at the shop. Testing it for the first time in a dark panel at 3 AM is a bad plan. · The backup schedule file. This is the .cnc file that RSNetWorx saves when you commission a network. If you do not have one, your night just got longer. If you have one but it is five years old, treat it with suspicion until you have compared it to the running network. · Physical spares: a short length of 1786-RG6 coax, two 75-ohm terminators, one spare tap, and a handful of BNC connectors. Take a full drum of cable if the trunk is long or runs outdoors. · A known-good 1756-CNB or 1756-CNBR, flashed to the firmware your plant runs, in case step 6 becomes necessary. · A multimeter, a flashlight, a small mirror for reading node addresses behind panels, and the EDS files for every third-party device on the net, carried on a USB stick.   Run the ladder in this order   ControlNet faults fall into four bins: the cable, the module, the schedule, and the node. The failure modes look alike from the operator screen, and that is the trap. A node that dropped because a terminator is missing looks identical to a node that dropped because its address collides with another node. The order of attack is not a preference. Check the physical layer first, then the module, then the schedule, then the node, and swap hardware last. Each step eliminates a whole class of faults, and none of them requires you to trust the story the operator told you at 2 AM.   Step 1: Check the physical layer first   ControlNet is a scheduled, time-sliced network running 5 Mbit/s on 75-ohm coax. Every node gets a guaranteed slot in a repeating frame, and the whole scheme depends on the signal arriving clean at every tap. Reflections kill that signal, and reflections come from bad geometry: open ends, wrong cable, stubs, water. Most "the net went down at 2 AM" calls end here, in the cable, not in the schedule. Start at one end of the trunk and work your way to the other. Power down what you can before you touch coax. Do not hot-unplug a live trunk while the plant is depending on it, and never pull a connector to "see if it sparks." It will not spark, and you will have just dropped the net. Check the terminators first. A ControlNet trunk needs exactly two, one at each physical end, and both must be 75 ohm. The 1786-XT is the correct part for this system. A missing terminator leaves the end of the cable open. The signal reflects off that open end, and nodes near it go marginal and drop when the cabinet warms up or a large motor starts. An extra terminator is just as bad when it hangs off a tap in the middle of the trunk, because it turns a healthy segment into two stubs. The rule is short: two terminators, at the ends, nothing else on the cable. Check every BNC connector on the trunk. Seated means you feel it click into place and you cannot rotate the shell against the jack. A connector that spins is a crimp that failed years ago and has been getting worse since. Look at the center pin. It should be clean, straight, and fully engaged. Water in a connector reads as intermittent loss that no schedule change will ever fix, and corrosion on the shield braid does the same. When you find a bad connector, cut it off and re-terminate with a fresh one rather than tightening it and hoping. Check the cable itself. The trunk must be 1786-RG6 quad-shield coax. RG-59 will carry the signal a short way and then lie to you, and the leftover TV coax someone used to patch a broken section is worse than no patch at all, because it passes the DC checks and fails under load. If someone spliced the trunk with a barrel connector, that splice is a reflection point and a future 2 AM call. If someone daisy-chained from one module's BNC straight to the next module's BNC instead of using taps, you are looking at a stub that should never have been built. Devices attach through taps, with a short drop cable from the tap to the node. Keep every drop to a meter or less and route it clear of power cables. Then run the numbers. A single ControlNet segment is limited to 1000 m of RG-6 and 48 nodes. If your plant exceeds either limit, a repeater must sit in the path, and the problem node is probably on the far side of that repeater. Look for the repeater and check its power before you go any deeper. While you are walking the cable, look for the obvious damage: coax crushed behind a swing panel, cable routed through a drain, water standing in a below-grade pull box, a fork truck scar on the jacket. ControlNet cable failures are rarely mysterious once you look at the actual cable. If the whole net will not come up, you are hunting a short or an open. Every node's network LED dark or flashing at the same time means the trunk is the problem. It is not forty modules that all failed in the same hour. Isolate the fault methodically. Power down nodes one at a time, pull their drops at the tap, and watch whether the rest of the net comes solid green. When you pull the drop that fixes the net, you have found the guilty piece. It is usually a crushed cable, a wet connector, or a tap that took a hit from a ladder. Fix that one thing and the net comes back whole.   Step 2: Read the module LEDs   The 1756-CNB and 1756-CNBR tell you a lot from the front panel if you read the indicators in pairs. The 1756-CNB carries two indicators, one for module status and one for network status. The 1756-CNBR carries three: module status plus one per redundant channel. The module LED tells you whether the hardware is alive. The network LED tells you whether it is talking. Read the module LED first. A module that is dead on the backplane will never talk on the net, no matter how good the cable behind it is. Indicator | Pattern | What it means | What to do Module LED | Off | No power, or the module is not seated on the backplane | Reseat the module firmly. Check the chassis power supply and the slot. Module LED | Solid green | Normal operation | Nothing. Move to the network LED. Module LED | Flashing green | Self-test in progress, or firmware being updated | Wait. If it still flashes after ten minutes, cycle power to the chassis. Module LED | Flashing red | Recoverable fault, usually configuration or firmware related | Check the firmware revision against the I/O tree in Studio 5000. Cycle power. Module LED | Solid red | Unrecoverable fault | Reseat once. If the red returns, the module is dead. Go to step 6. Network LED | Off | Module is alive but not talking on the trunk | Check the tap, the drop cable, and the trunk behind this node. That is step 1 work. Network LED | Solid green | Online and passing scheduled traffic | Normal. Nothing to do. Network LED | Flashing green | Powered but not communicating with the network | The node cannot hear the net. Check the terminator, the tap, and the node address. Network LED | Red, solid or flashing | Duplicate node address, or a serious network fault | Power the node down. Check its address against every other node. Check the trunk. On a 1756-CNBR running redundant media, the two network indicators should mirror each other. One solid green while the other shows red means the fault lives on that channel's cable or terminator, not in the module. Swap the suspect channel's cable and terminator before you condemn the module, and you will save yourself a part. One field rule carries you a long way. When every node on the net misbehaves at the same time, it is the trunk. When exactly one node misbehaves and the rest sit solid green, it is that node, its tap, its drop, or its address. Make that split early and you will not waste an hour working the wrong end of the ladder.   Step 3: Go online with RSNetWorx and verify the schedule   Get RSNetWorx for ControlNet online against the network before you change anything. Select the driver that matches your interface card, browse, and let the software discover the net. Write down what it finds: how many nodes, which ones are scheduled, which ones are not. That list is your map for the rest of the night. Then settle the question of who owns the schedule. On ControlNet, the schedule is the arrangement of who talks in which time slot. It lives in two places. The .cnc file holds it on whoever commissioned the network, and every scheduled node holds a copy of its own part. When RSNetWorx goes online and its file disagrees with the network, it asks which one to keep. If the network has been running fine and your file is stale, upload from the network and save it under a fresh name. If the network is the mess you were called to fix and your file is the good one, restore from the file. Make that decision once, deliberately, and say it out loud before you click. The wrong choice wipes a working schedule, and nothing in RSNetWorx will warn you twice. Open the network properties and read two numbers: the NUT and S_max. The NUT, or network update time, is the length of the repeating frame that carries all scheduled traffic. The default is 2 ms, and most plants never need more. S_max is the highest node address the schedule will accommodate. It must sit above your highest scheduled node. If someone added a node at address 60 while S_max sat at 50, that node will never be scheduled, no matter how many times you commission. Raise S_max, then commission. This one setting has sent more engineers in circles than any cable fault I have seen. RSNetWorx also shows the split between scheduled and unscheduled bandwidth. Scheduled traffic gets a guaranteed slot in every frame. Unscheduled traffic, the explicit messages, uploads, and programming traffic, fills whatever space is left. When a new connection will not fit the schedule, RSNetWorx tells you plainly. The fix is a larger NUT or fewer scheduled connections, never magic and never a second commission with the same numbers. While you are online, look at each scheduled node. RSNetWorx marks devices that are present but missing from the schedule, and it marks devices it cannot identify. Both conditions show up here first, and both have different fixes. If the net looks healthy in RSNetWorx, the problem is narrower than the phone call suggested, and step 4 will find it.   Step 4: Find the missing node   The plant says node 14 is gone. RSNetWorx says it sees 47 of 48 nodes. Do not trust the node number painted on the panel door. Trust the address the device is actually set to, because the two have disagreed since the day the panel was built. First, confirm the address. A 1788-CN2DN takes its node address from the switches on the device, and valid addresses run from 1 to 99. Write down what the switches actually say, not what the drawing says. A 1756-CNB holds its address in software, set through RSLinx or the module properties in Studio 5000. If the device's real address does not match the address the schedule expects, RSNetWorx will show the device sitting there healthy while the schedule ignores it completely. That mismatch produces exactly the phone call you got. Second, check for a duplicate. Two nodes on the same address is the classic intermittent fault. Both power up, one wins the slot, the other drops, and the drop rotates between them on every restart. If the missing node comes back the moment you power down its neighbor, you have a duplicate address. Change one node to a free address and re-commission. Do not put it off, because the duplicate will come back the next time both devices power cycle. Third, look at the tap. The drop cable from tap to node must be seated at both ends, and the node end is the one everybody forgets because it hides behind the module's own connector. A BNC that spins at the node end means a failed crimp. Replace the whole drop rather than re-crimping the old one, because the old one has been flexing for years and will fail again. Confirm the tap body itself is the right one for your trunk and that its clamp is actually closed on the coax. A tap that was installed but never tightened is a node that works until the cabinet door slams. Fourth, sort out what RSNetWorx is telling you, because its display is precise if you read it right. A device that appears as a question mark is present but unidentified. Its EDS file is missing from the machine running RSNetWorx, so the software cannot read its identity. Install the EDS file and refresh the browse. A device that appears with a name but no scheduled connections is not in the schedule, and that is step 5's problem. A device that does not appear at all is a physical problem, and that is step 1's problem. Work the step that matches the symptom. While you are standing at the node, look at the device itself and not just its connector. A 1788-CN2DN with a shorted DeviceNet side will drag down its ControlNet side, because the two share one processor. Check the node's own power supply as well. A drive or a linking device that is running on a dying 24 VDC supply will drop off the net in a pattern that looks exactly like a network fault. Put a meter on the node's supply terminals before you blame the trunk, and check it under load, not in a quiet moment between cycles.   Step 5: Fix the schedule and re-commission   Once the node is physically present and correctly addressed, the fix is to put it back into the schedule and write that schedule to every node on the net. That write is called commissioning, and it is the point of no return in RSNetWorx, because it downloads to every scheduled node at once. Start from the file. Open your backup .cnc and go online. If the backup is older than the running schedule, upload the running schedule first and save it under a new name before you touch anything. Then compare the two files and understand the difference. What you are about to do will overwrite the network, so you want to know exactly what you are overwriting and why. Put the network into edit mode in RSNetWorx, then look at what connections the controllers are requesting. This is the part that trips people up. The ControlNet schedule is built from connections the controllers actually request, and those requests come from produced and consumed tags that already exist in the controller logic. If the tag was deleted from the program months ago, no schedule entry in RSNetWorx will fix it. The connection has to be requested from the controller side first. Check the program in Studio 5000 before you blame RSNetWorx, and confirm the produced or consumed tag is still there, still enabled, and still mapped to the right node. With the connection requested and the node online, add the node to the schedule, confirm that S_max covers its address, and commission. RSNetWorx computes the schedule and downloads it to every scheduled node in one pass. Expect scheduled I/O to blip for a few seconds during the download. That blip is why you do this in a planned window when the line can afford it, not while the process is mid-batch. Verify after commissioning. Every scheduled node should sit solid green on its network LED. RSNetWorx should show a clean schedule with no unscheduled stragglers. The controller's I/O tree should show the connection running, and a test bit should actually move end to end. Then save the .cnc file, name it with the date, and put it somewhere the next shift can find it without calling you. Here is the lesson every ControlNet veteran has paid for at least once. The .cnc file is the network. Lose it, and a dead module becomes a two-day project, because a replacement module has to be added to a schedule that no longer exists anywhere except in the heads of people who have left the company. If you have no .cnc file at all and the net is currently running, go online right now and upload the schedule to a file. Do it before something dies, not after. Rebuilding a schedule from scratch means matching every produced and consumed tag in every program against physical nodes, and that job is always done once, at night, badly.   Step 6: Swap the module when it is dead   You have a 1756-CNB with a solid red module LED that survives a reseat and a power cycle. The module is dead, and the schedule is fine. Replace it. Before you pull it from the rack, record two things: the node address and the firmware revision. Both are cheap to read now and expensive to guess later. Get the address from RSLinx or from the module properties in Studio 5000. Get the firmware revision the same way, or from RSNetWorx while you are online. Then pull the old module and install the replacement in the same slot. Set the new module's address to match the old one before it joins the net. A fresh module sits at its default address until you tell it otherwise, and two modules sitting at the same default on the same network will fight exactly the way step 4 described. Flash the firmware with ControlFlash until it matches the revision the plant runs. If the I/O tree in Studio 5000 uses exact-match electronic keying, a revision difference will fault the connection even though the hardware is perfectly good. Attach the trunk, apply power, and watch the LEDs run through the sequence in step 2. The module LED should go solid green. The network LED should go solid green once it is passing traffic. Then go online with RSNetWorx and expect the new module to appear as a stranger standing at the old address. That is normal. If the schedule does not pick it up, commission from your backup .cnc exactly as you did in step 5, and verify the connection moves data before you call the job done. Keep the dead module out of the rack and decide what to do with it on a normal workday. A repaired module that fails again at 2 AM erases whatever you saved on the repair cost. Where does the spare come from? Not from the local distributor's shelf, because most distributors stopped stocking 1756-CNB modules the day Rockwell moved on. You keep one on your own shelf, tested and flashed, or you buy from a supplier that specializes in legacy Allen-Bradley hardware. That choice is the difference between a forty-minute swap and a week of expedited freight. The Allen-Bradley stock at tztechio.com is one place to look, and your own shelf is the better place to keep it.   Quick reference: symptom, cause, fix   Symptom | Likely cause | Fix Whole net down, every network LED dark or flashing | Missing or shorted terminator, water in the trunk, a tap drop shorting the segment | Step 1: check both terminators, then isolate taps one at a time One node drops at random and returns when it cools off | Marginal terminator, corroded BNC, failing node power supply | Step 1: reseat connectors, replace the drop, verify node power under load One node never appears in RSNetWorx | Address conflict or a dead tap | Step 4: read the actual address switches, walk the tap Node appears as a question mark | EDS file missing from the RSNetWorx machine | Install the EDS file, refresh the browse Node present but carrying no scheduled traffic | Node not in the schedule | Step 5: add the connection, commission Module LED solid red after reseat and power cycle | Dead module | Step 6: swap it, match firmware and address Net healthy but the controller faults the connection | Schedule changed under it, or module revision mismatch | Steps 5 and 6: re-commission, check electronic keying   ControlNet in 2026: run it, but plan the exit   Here is the honest picture. Rockwell's lifecycle status for ControlNet is Active-Mature. Support continues, and the installed base is huge, but new development stopped years ago and the catalog gets thinner every year. The company's direction is EtherNet/IP, and the 1783 family of switches and infrastructure is where new work goes. If you are designing a greenfield line, use EtherNet/IP and do not look back. Most of you are not designing a greenfield line. You are keeping a line that paid for itself years ago running while the plant decides what comes next. A migration off ControlNet is a real project with its own risks, and it does not happen at 2 AM when a node drops. If you are staying on ControlNet for another five years, run it like the critical utility it is: current drawings, tested spares, backed-up schedule files, and one named person who owns the network. If you are migrating, do it in a planned outage, prove the new path under real load, and keep the ControlNet trunk in place until the new one has earned your trust. Do not cut over on faith. The coax has carried this plant for two decades; the new network gets to prove itself before the old one is scrapped. For the racks that stay, the practical question is parts. ControlNet modules, coax, taps, and terminators are no longer made in the volumes they once were, and the PLC spares market is where legacy racks get fed. Buy what you need while it is findable, and treat the purchase as insurance rather than expense.   The spares shelf   Minimum shelf stock for one ControlNet network looks like this. One 1756-CNB or 1756-CNBR per network, flashed to the firmware your plant runs and tested before it goes on the shelf. One 1788-CN2DN if your net feeds DeviceNet through a linking device. A 30 m reel of 1786-RG6 coax, a handful of BNC connectors, and four 75-ohm terminators, because you will lose two before you need one. One spare tap of the style your panels actually use. The maintenance laptop, with RSNetWorx installed, the interface card tested, and every EDS file loaded. And the .cnc backups, on two different USB sticks, one of which lives inside the panel in a labeled bag. Check that shelf twice a year, in daylight, when nothing is broken. Test the spare modules in a live rack so you know they work. Refresh the USB sticks when the schedule changes. ControlNet is Active-Mature, which means the parts are not getting easier to find, and the industrial automation suppliers that still carry this generation of hardware are worth knowing before you need them, not after. Do the steps in order, keep the spares on the shelf, and keep the backup file where you can reach it at 2 AM. That is the whole job. The net will drop again. The question is whether you are ready for it the second time. URL Slug: controlnet-troubleshooting-guide -------------------------------------------------------------------------------------------- 🏢 About TZ Tech   TZ Tech is a leading supplier of industrial automation, electrical, instrumentation, and telecommunications components. We specialize in sourcing ready-to-ship distributor stock, allowing us to offer highly competitive pricing and short lead times. Thanks to our extensive inventory, we can even source rare and discontinued parts that are hard to find elsewhere.   🛡️ Our Quality Commitment   We understand that quality is your top priority. Every component undergoes a strict screening and inspection process so you can buy with absolute confidence. For legacy or discontinued parts, we believe in complete transparency and will always provide an honest, accurate report on the product's condition. Plus, all brand-new parts come backed by a full 1-year warranty.   ✉️ Get in Touch     Have a project or a part you need? Send us your inquiry today! Our team is dedicated to providing a fast response within 6 hours (excluding weekends).  
Subscribe

Please read on, stay posted, subscribe, and we welcome you to tell us what you think.

submit
Copyright 2026 @ TZ TECH Co., LTD. .All Rights Reserved Disclaimer: We are not an authorized distributor or distributor of the product manufacturer of this website, The product may have older date codes or be an older series than that available direct from the factory or authorized dealers. Because our company is not an authorized distributor of this product, the Original Manufacturer’s warranty does not apply.While many DCS PLC products will have firmware already installed, Our company makes no representation as to whether a DSC PLC product will or will not have firmware and, if it does have firmware, whether the firmware is the revision level that you need for your application. Our company also makes no representations as to your ability or right to download or otherwise obtain firmware for the product from our company, its distributors, or any other source. Our company also makes no representations as to your right to install any such firmware on the product. Our company will not obtain or supply firmware on your behalf. It is your obligation to comply with the terms of any End-User License Agreement or similar document related to obtaining or installing firmware.

Sitemap | Blog | XML | Privacy Policy

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

Home

Products

whatsApp

contact

YOUR COOKIE SETTINGS

In addition, with your permission, we want to place cookies to make your visit anointeraction with slOC more personal. For this we use analytical and advertisingcookies. With these cookies we and third parties can track and collect yourinternet behawior inside and outside super-instrument.com. With this we and third parties adapt super-instrument.com and advertisementsto your interest. By clicking Accept you agree to this. If you decline, we only usethe necessary cookies and you unfortunately will not receive any personalizedcontent. Please visit our Cookie policy for more information or to change yourconsent in the future.

Accept and continue Decline cookies